Customer drawings
into production
tooling.
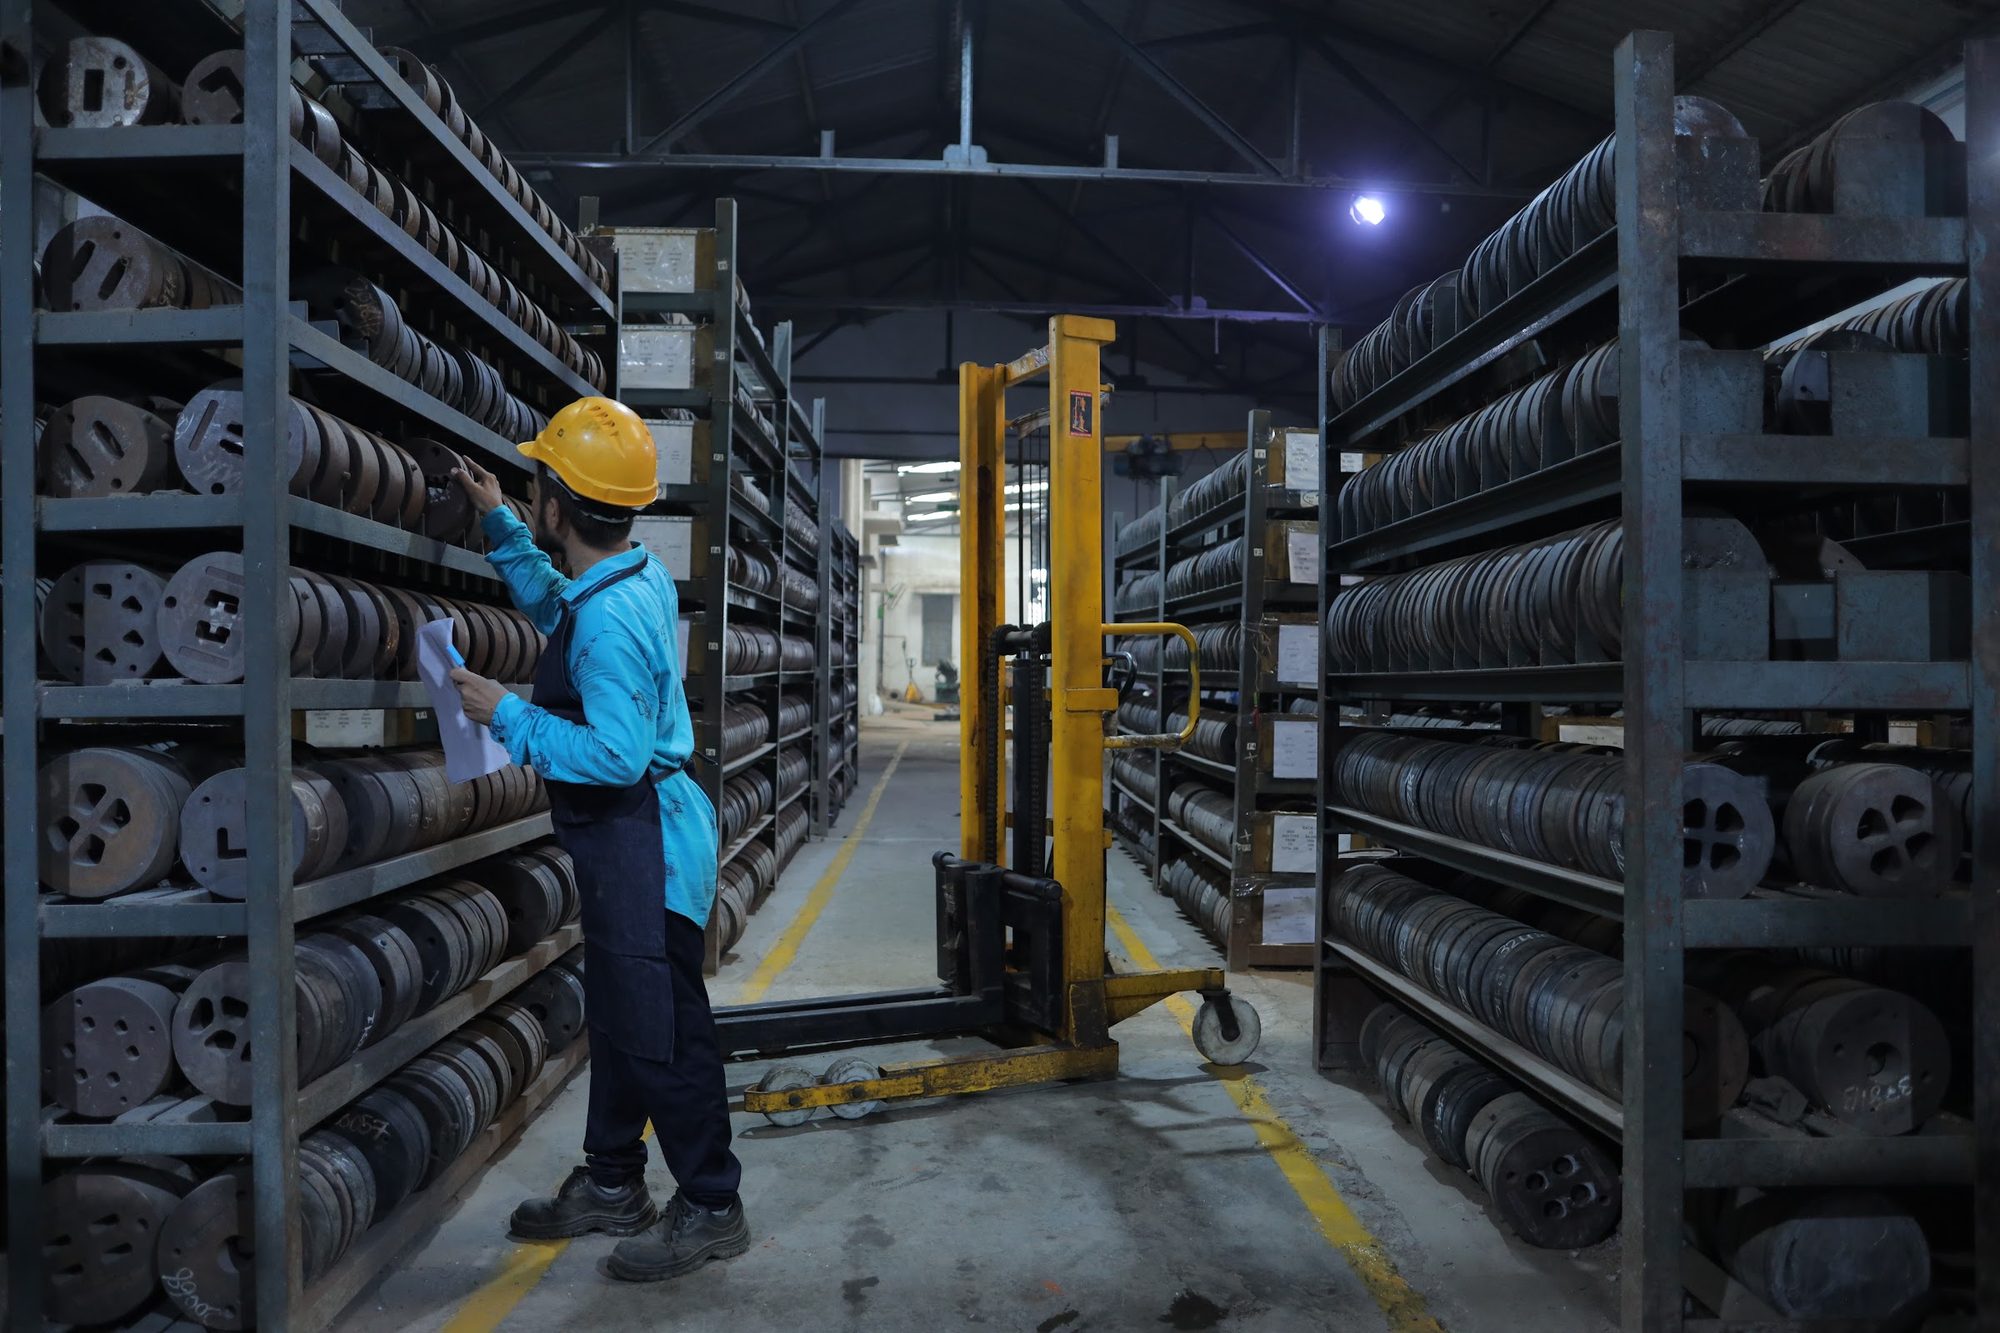
Banco's in-house Die Shop manages complete tooling for all five presses, from QForm flow simulation to trial extrusion and sample approval. Standard profiles have a typical 2–3 week die lead time, while critical or complex profiles are scheduled based on die and tooling complexity.
Four stages from
drawing to trial.
Every die goes through a structured design and validation process before a single billet is loaded. Q-Form simulation eliminates the majority of first-off failures and reduces sampling iterations.
Drawing review
Customer drawings are reviewed for extrudability and potential complexities, including wall thickness, tongue ratio, and circumscribed circle diameter. Modifications are suggested where required to improve reliability, die life, and surface finish.
Q-Form simulation
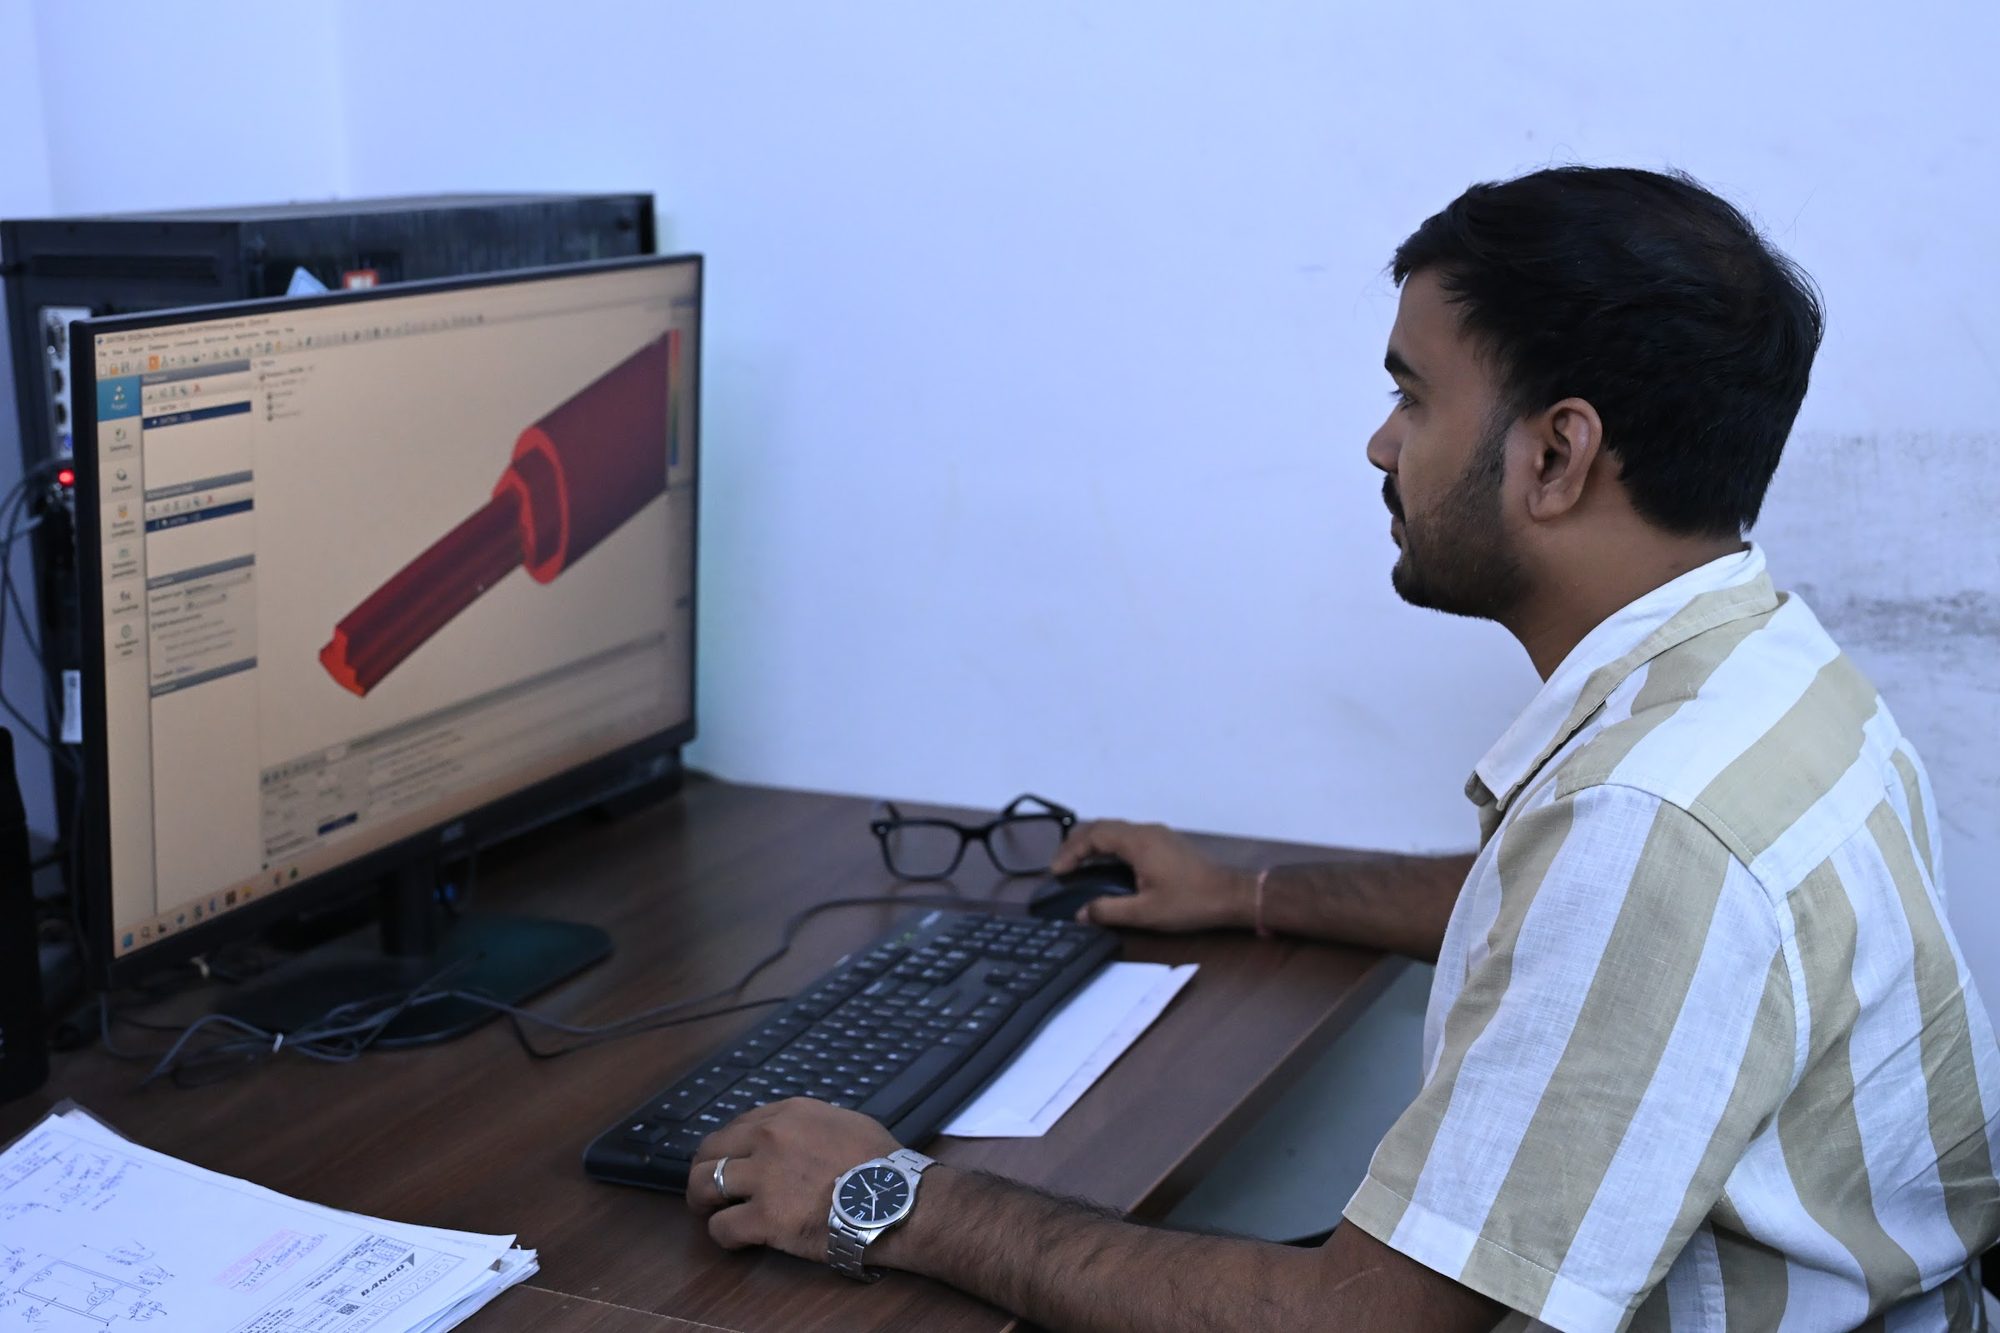
Designs are converted into 3D models and simulated using QForm – UK software to predict metal flow, temperature distribution, weld seams, and deflections.
Die manufacturing
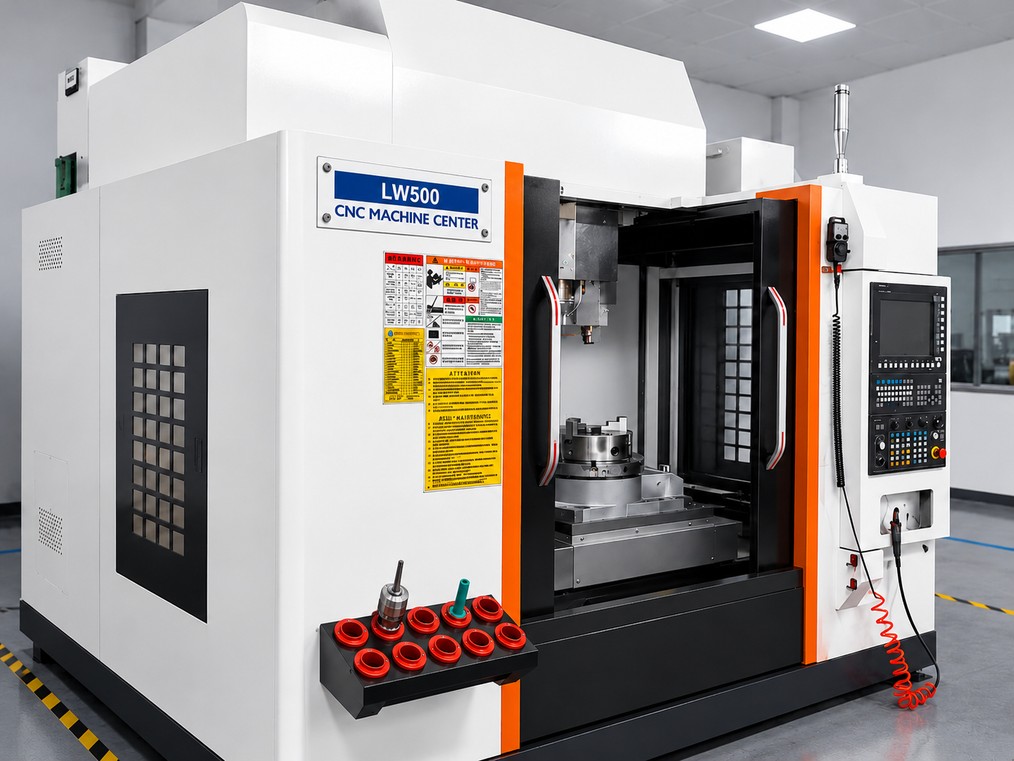
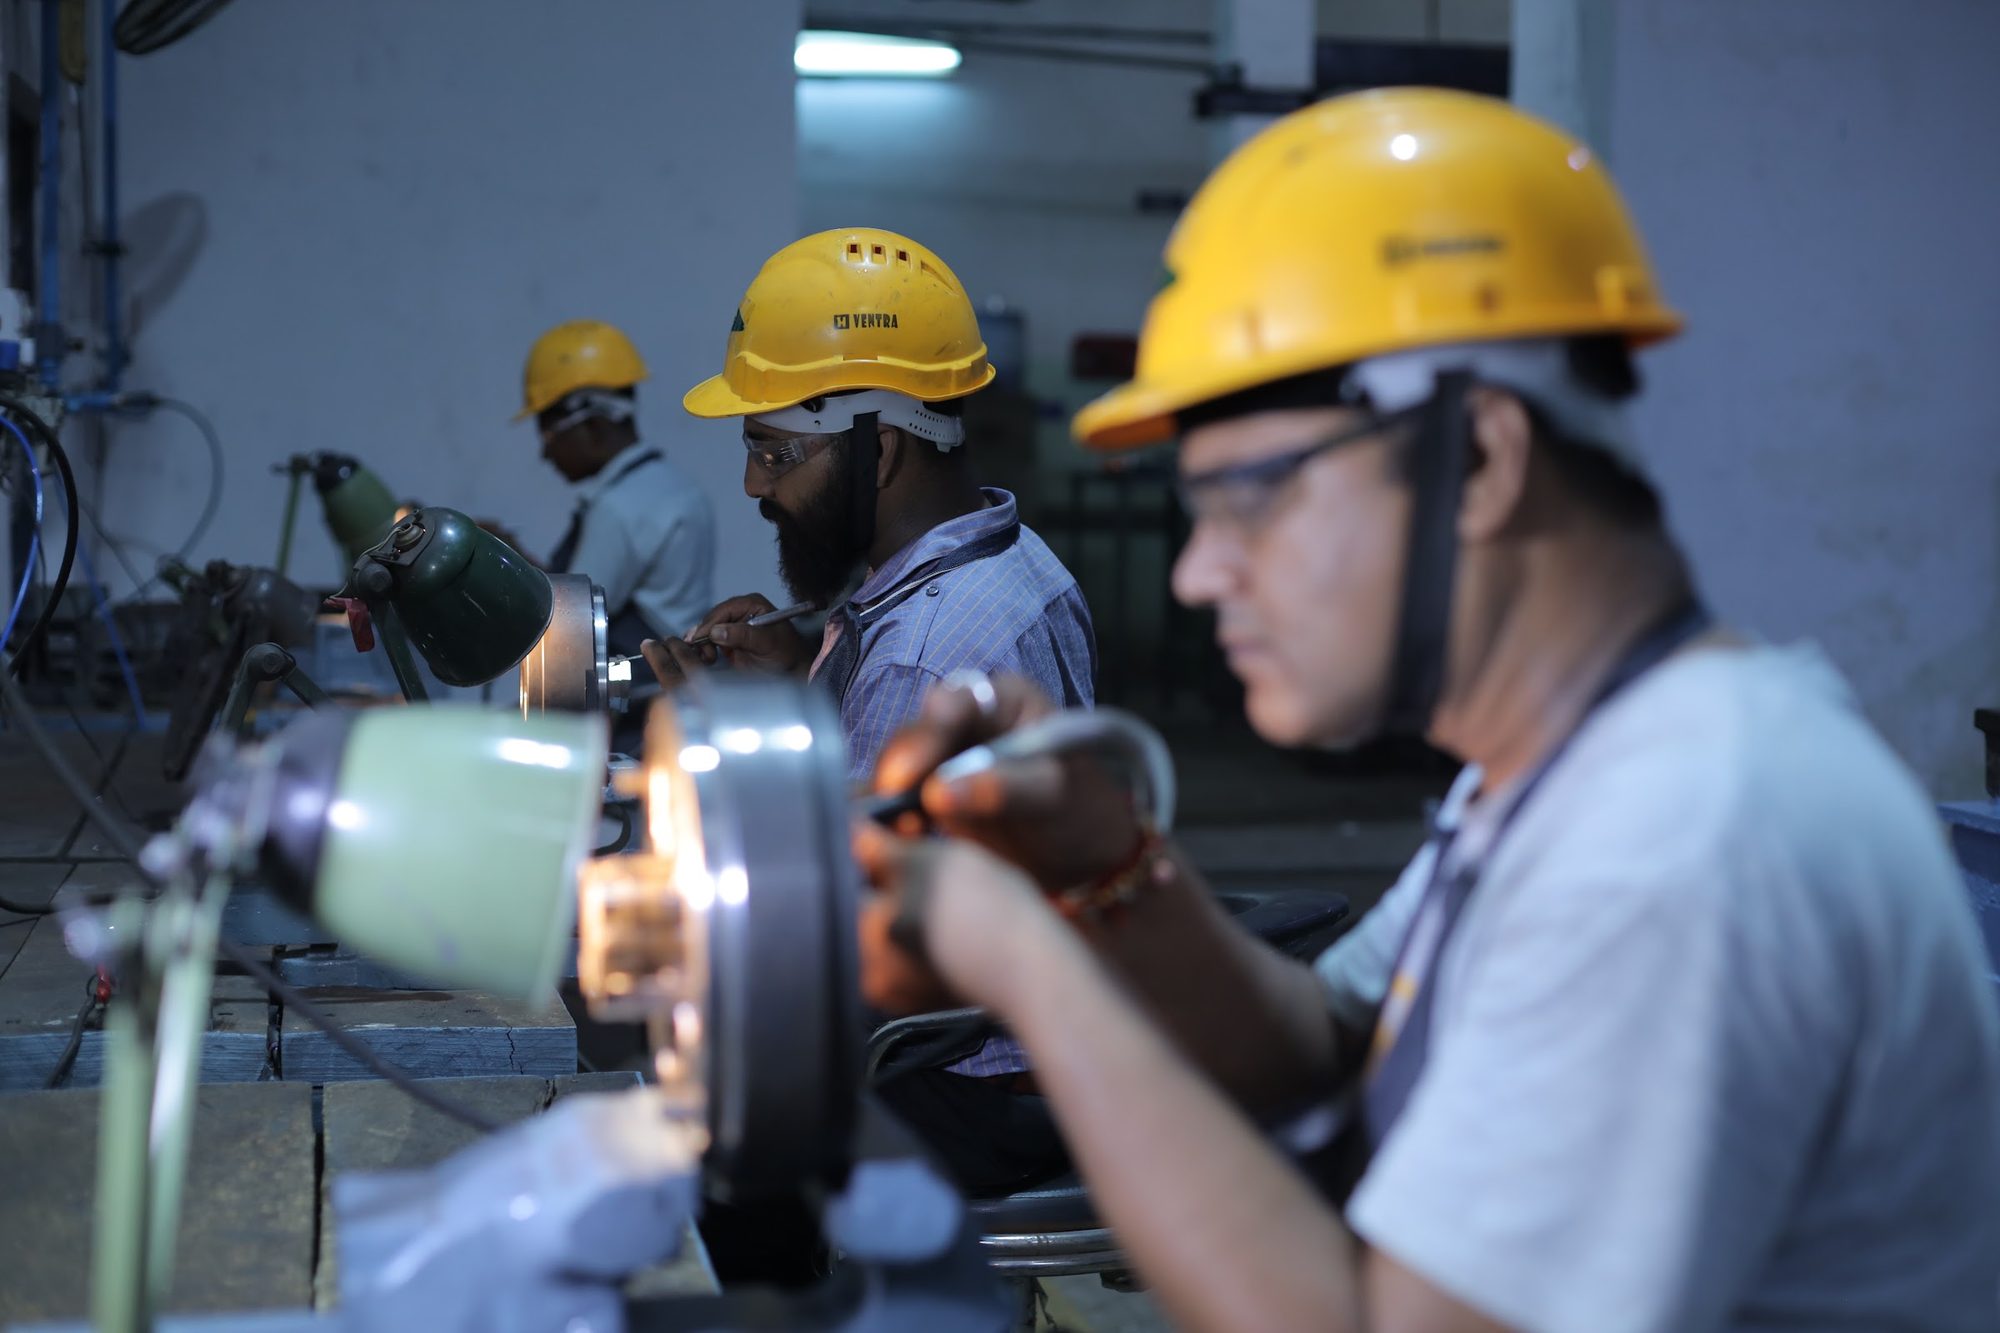
Manufacturing starts immediately using ready-stock raw materials, followed by CNC machining, heat treatment, and inspection.
Trial
Ready dies are issued for trials, and samples are validated and submitted for customer approval.
5-axis CNC.
H13 tool steel.
Nitride hardened.
5-axis CNC machining reduces manual intervention, improves die consistency, and supports faster delivery. Majority of dies are manufactured from H13 hot-work tool steel, while critical dies use special-grade steels selected based on application and tooling requirements.