Standard alloys.
Hard alloys.
Lead-free grades.
Custom compositions.
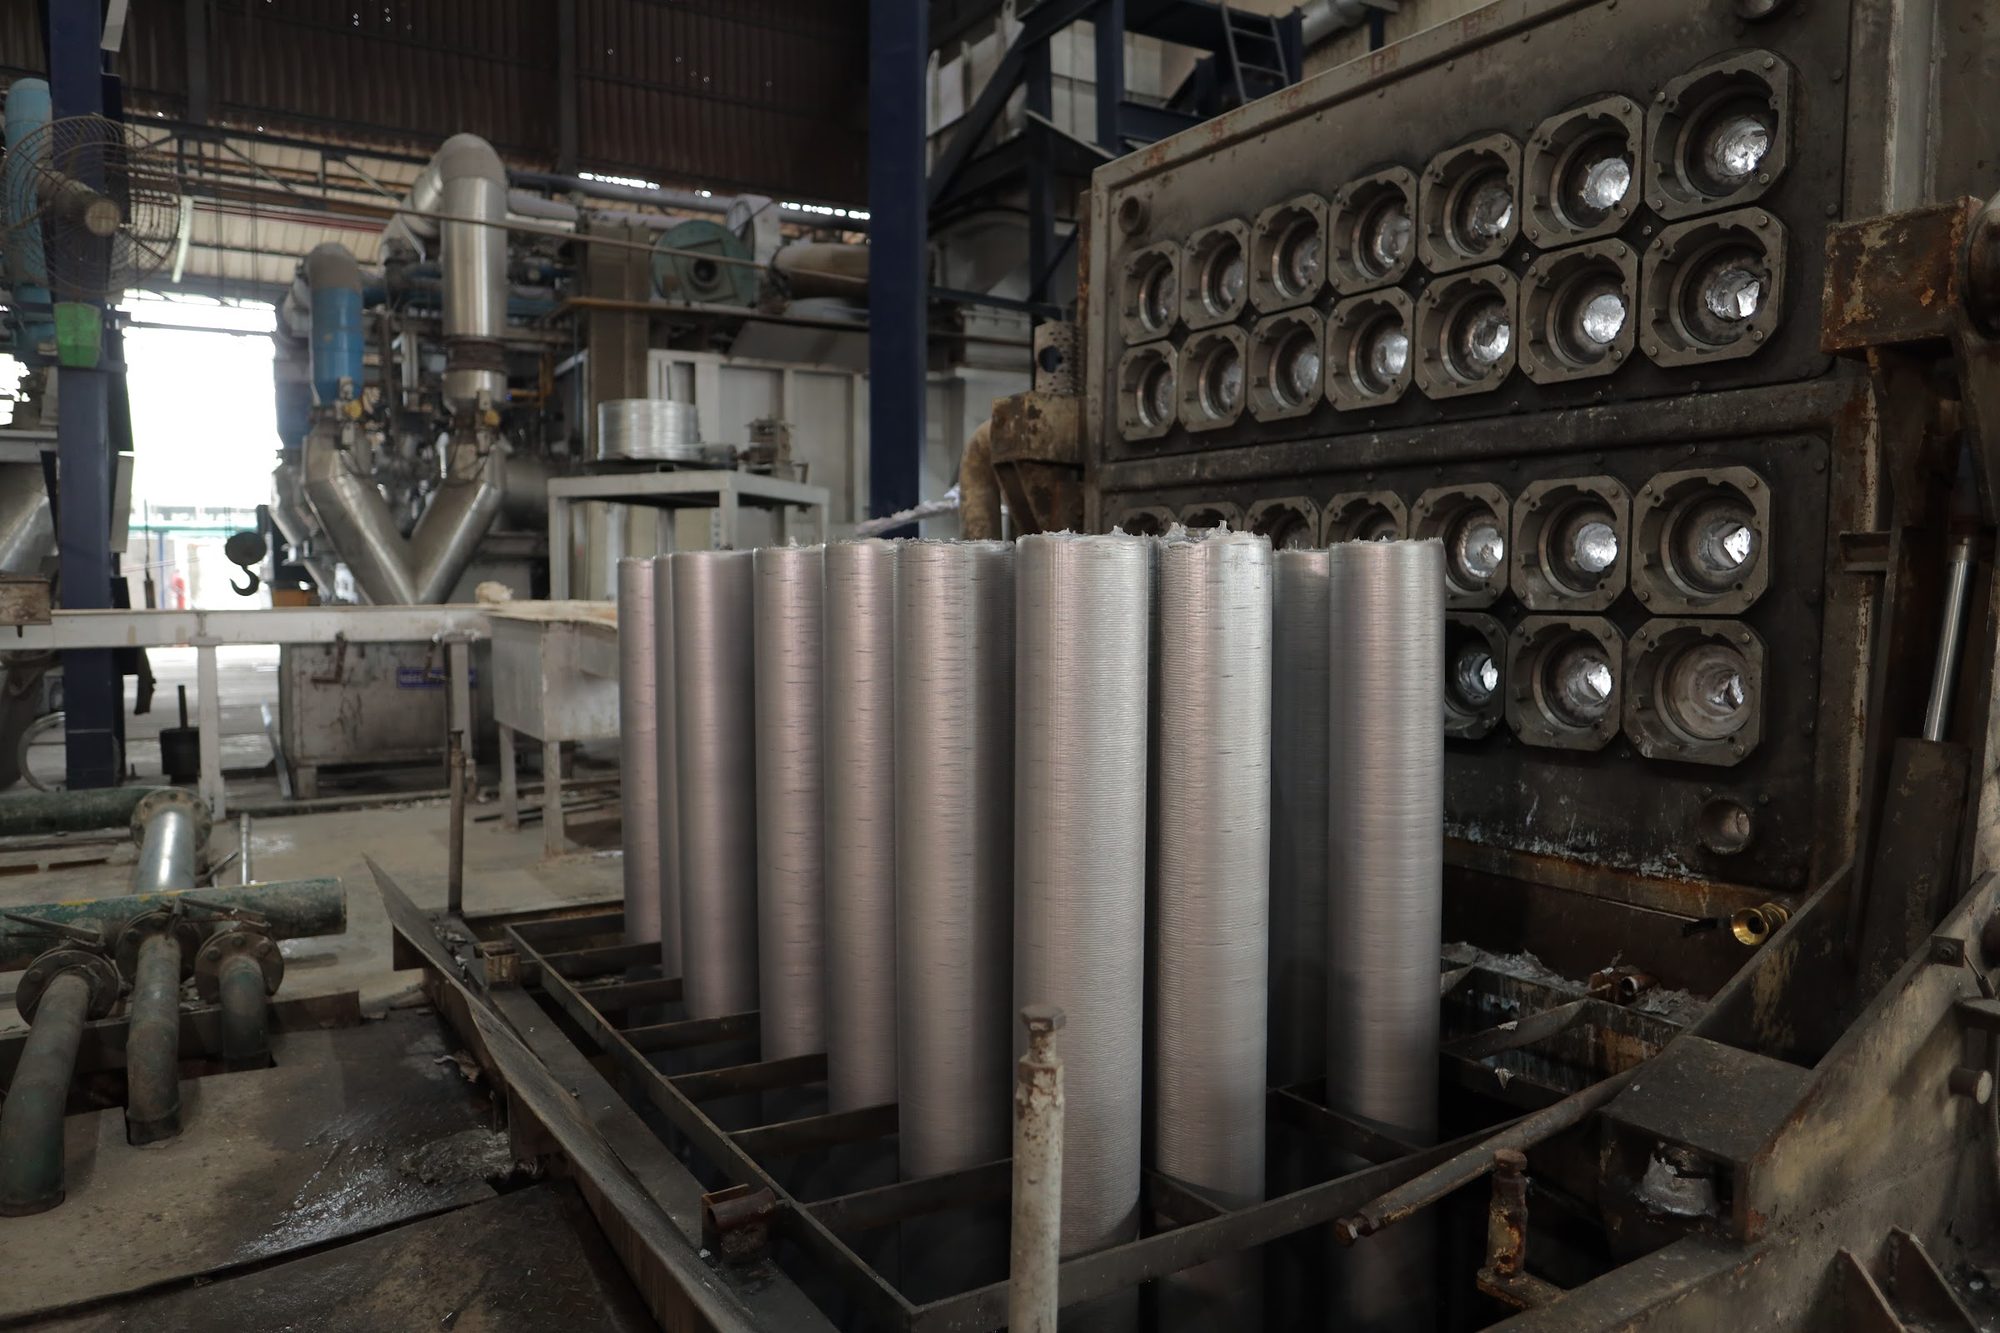
Banco's in-house foundry produces 55,000 MT of high-quality extrusion billets per year across all categories with homogenisation, giving downstream extrusion complete control over alloy chemistry, temper, and metallurgical structure.
Covering Every
Extrusion Application.
From soft alloys to complex hard alloys and RoHS-compliant machining grades, Banco's in-house alloy capability removes third-party dependency for chemistry and billet quality.
Hard alloys
High-strength alloys engineered for demanding structural and mechanical applications. More flexible and corrosion-resistant than steel, suited to safety-critical and load-bearing profiles where alloy chemistry and dimensional consistency are non-negotiable.
Lead-free machining alloys
Specifically formulated machining grades compliant with the RoHS directive. Designed for automated CNC machining operations where lead-containing alloys cannot be specified. Consistent chip-breaking characteristics and superior machinability.
Soft and medium alloys
The 1xxx, 3xxx, and 6xxx series for architectural, electrical, and general engineering. From food-grade packaging and utensils to building profiles, transport, and renewable energy structures. Versatile and weldable.
Controlled chemistry.
Cast to specification.
| Alloy | Si (wt%) | Mg (wt%) | Fe (wt%) | Cu (wt%) | Primary application |
|---|---|---|---|---|---|
| 1070A | ≤ 0.10 | ≤ 0.03 | ≤ 0.25 | ≤ 0.03 | Pure aluminium |
| 3003 | ≤ 0.10 | ≤ 0.05 | ≤ 0.25 | 0.05–0.09 | Heat exchanger · automotive |
| 6060 | ≤ 0.10 | 0.48–0.54 | 0.10–0.25 | ≤ 0.07 | Architectural profiles |
| 6063 | ≤ 0.10 | 0.48–0.55 | ≤ 0.30 | ≤ 0.10 | Windows · doors · general |
| 6082 | ≤ 0.10 | 0.72–0.79 | ≤ 0.30 | ≤ 0.10 | High strength structural |
| 6061 | ≤ 0.10 | 0.90–0.98 | ≤ 0.35 | 0.18–0.25 | Engineering · aerospace |
| 6066 | ≤ 0.10 | 1.00–1.10 | ≤ 0.30 | 0.80–0.90 | High-strength forgings |
Full compositions including Mn, Zn, Cr, Ti available in alloy data sheets. Additional grades (2011, 2017A, 2014, 5083, 6005A, 6101) produced on request.
Five controlled stages
from scrap to billet.
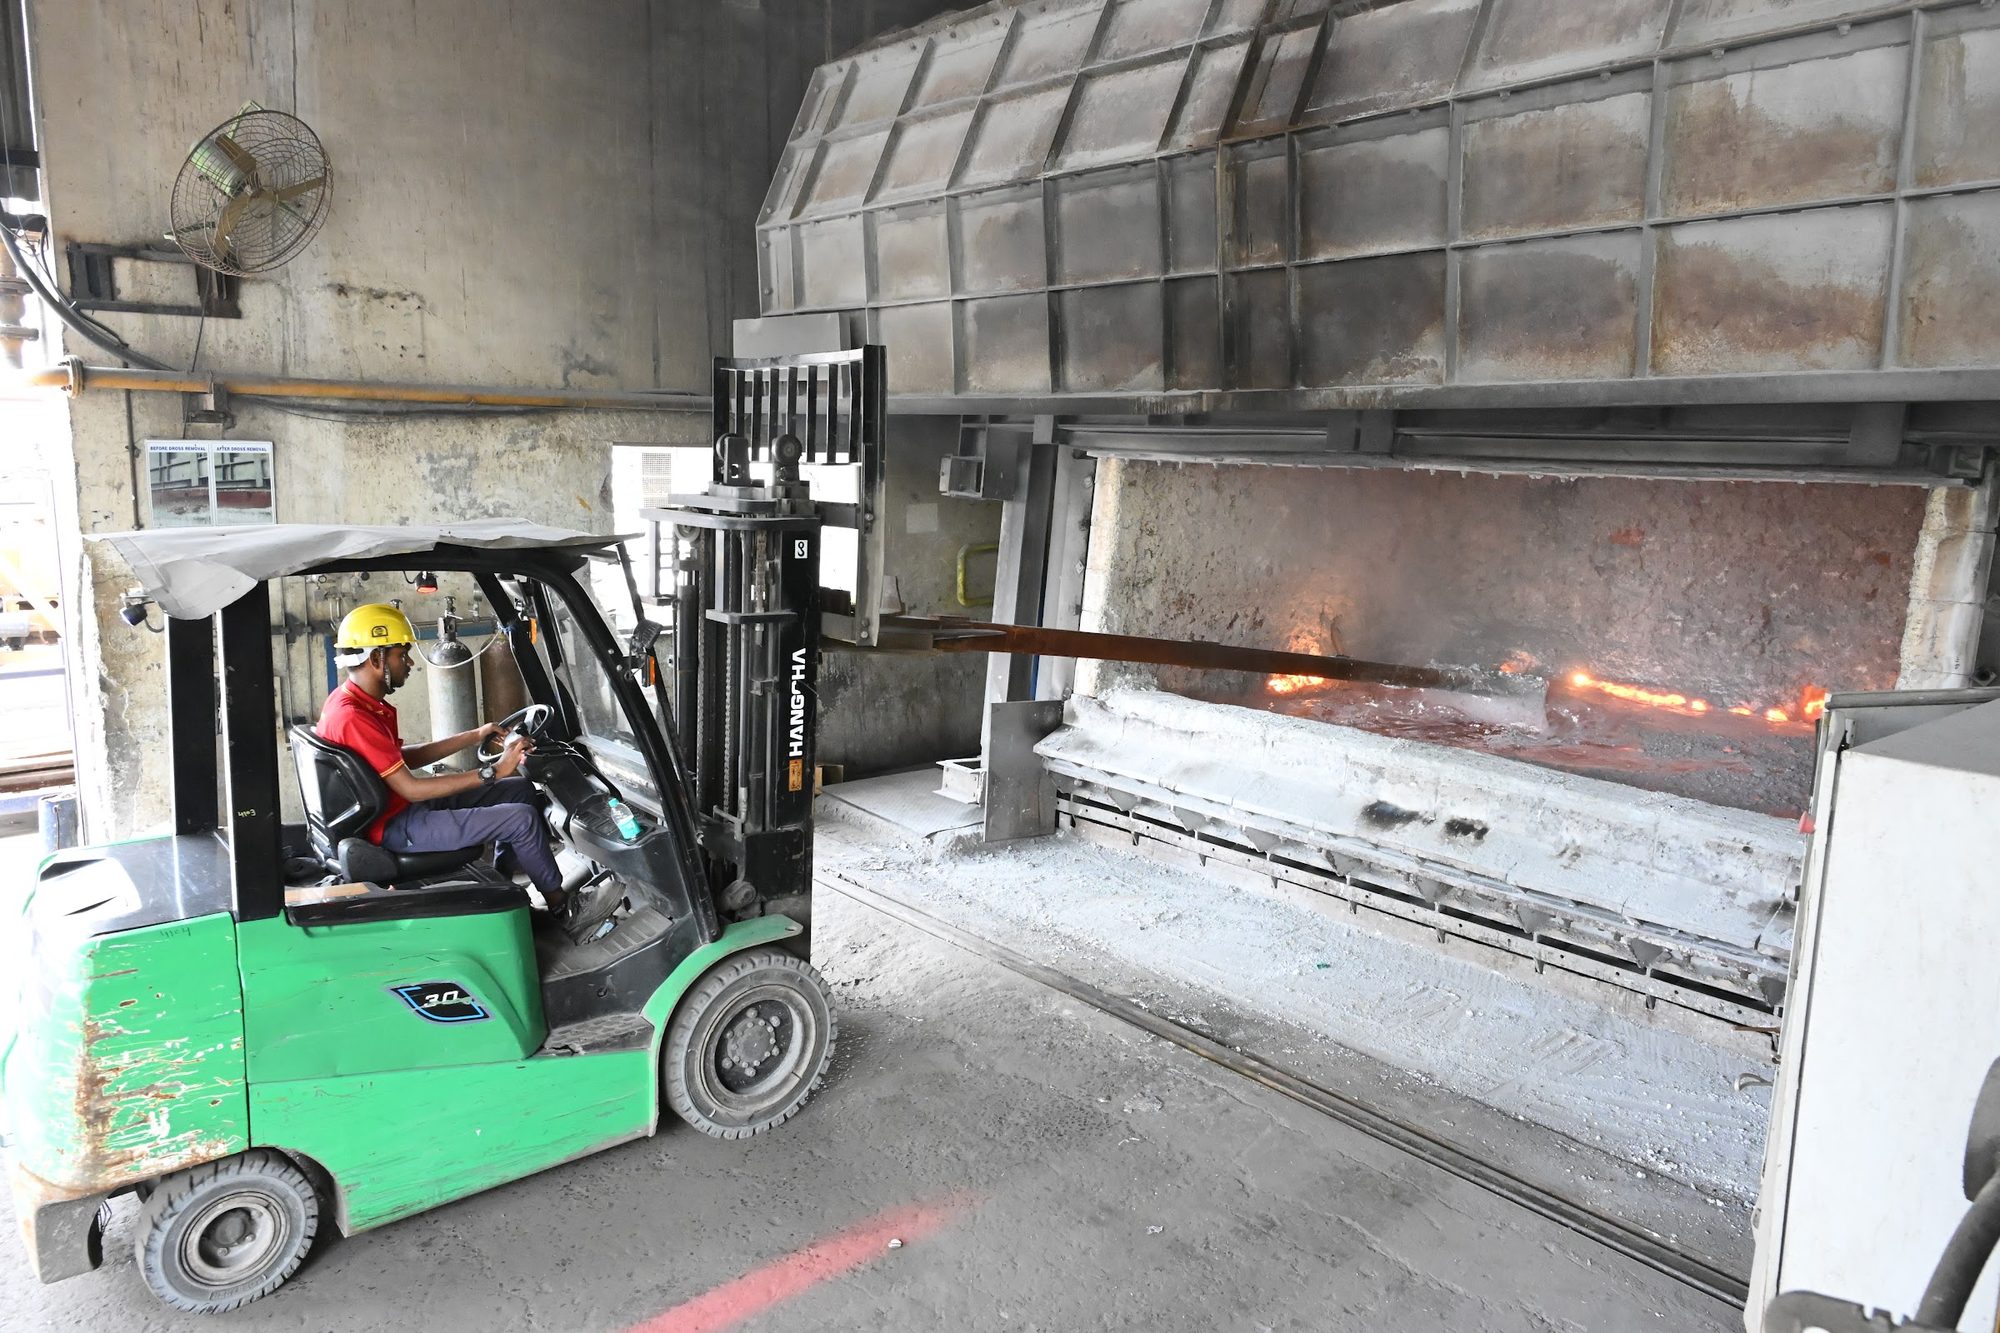
Melting
Charge materials are melted in gas-fired furnaces to a controlled tapping temperature, the starting point for consistent alloy chemistry batch after batch.
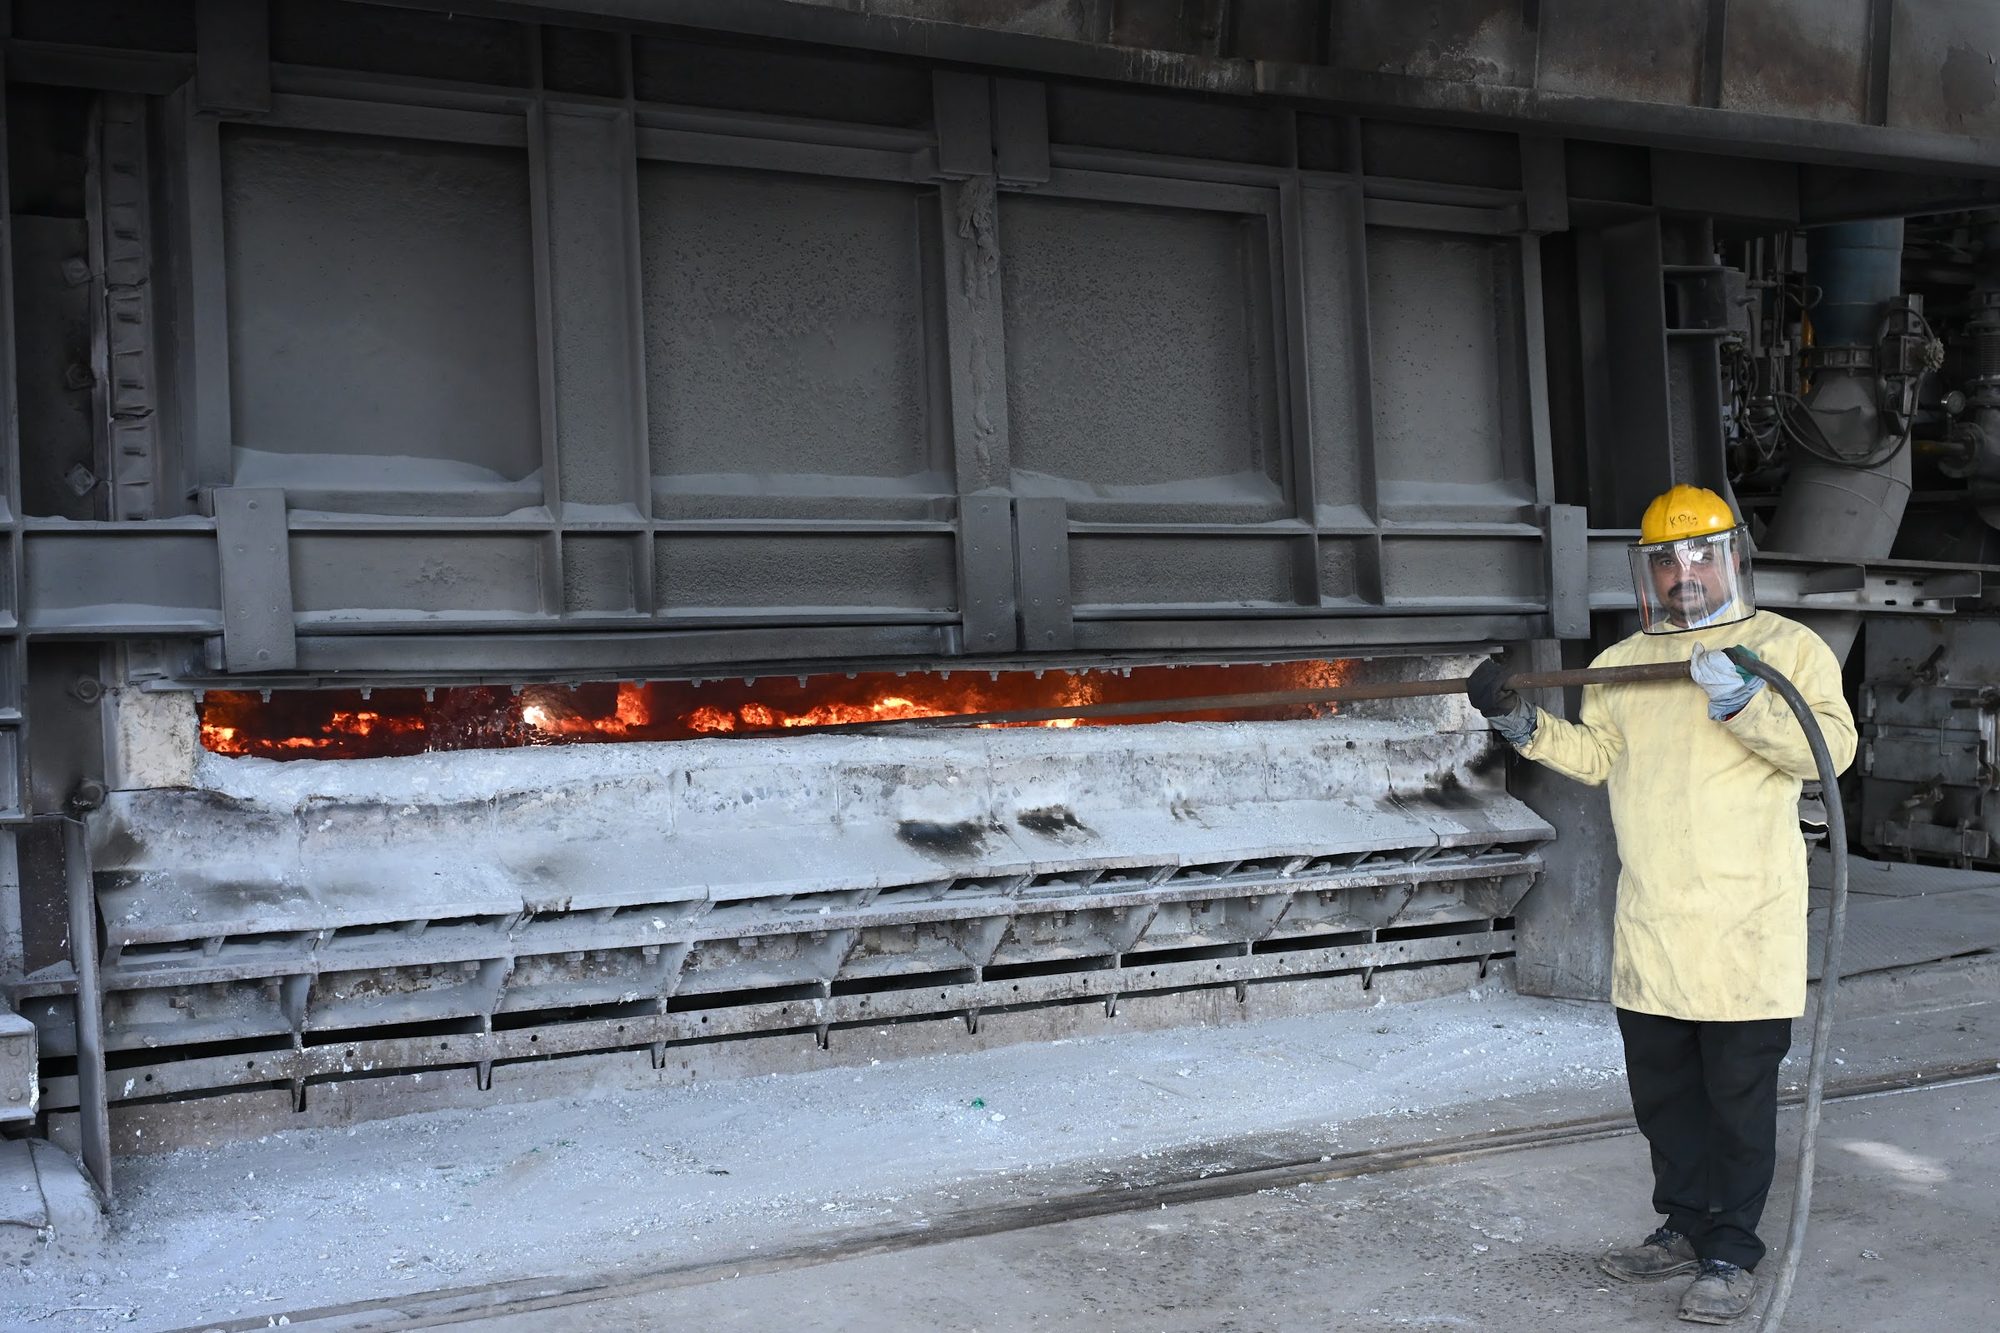
Refining & degassing
Nitrogen purging removes dissolved hydrogen from the melt, preventing porosity and surface blistering that compromise extrudability in downstream presses.
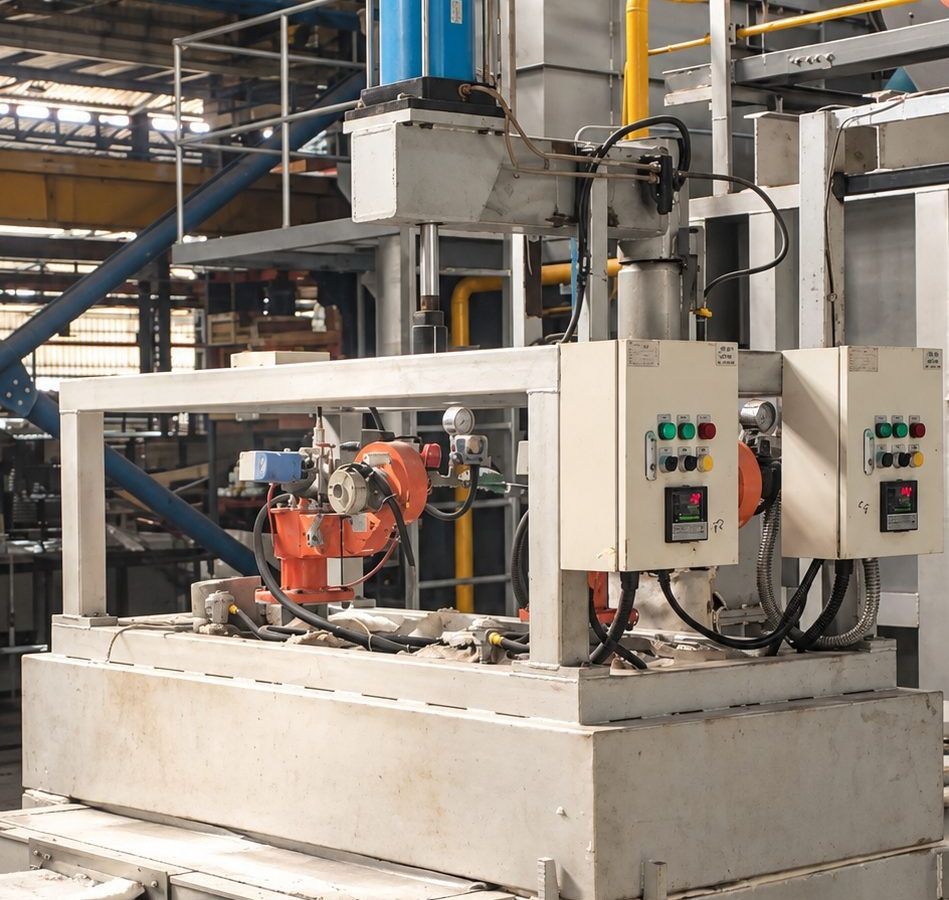
Ceramic foam filtration
Ceramic foam filtration removes non-metallic inclusions from the liquid metal before the casting station, improving metal cleanliness and reducing inclusion count.
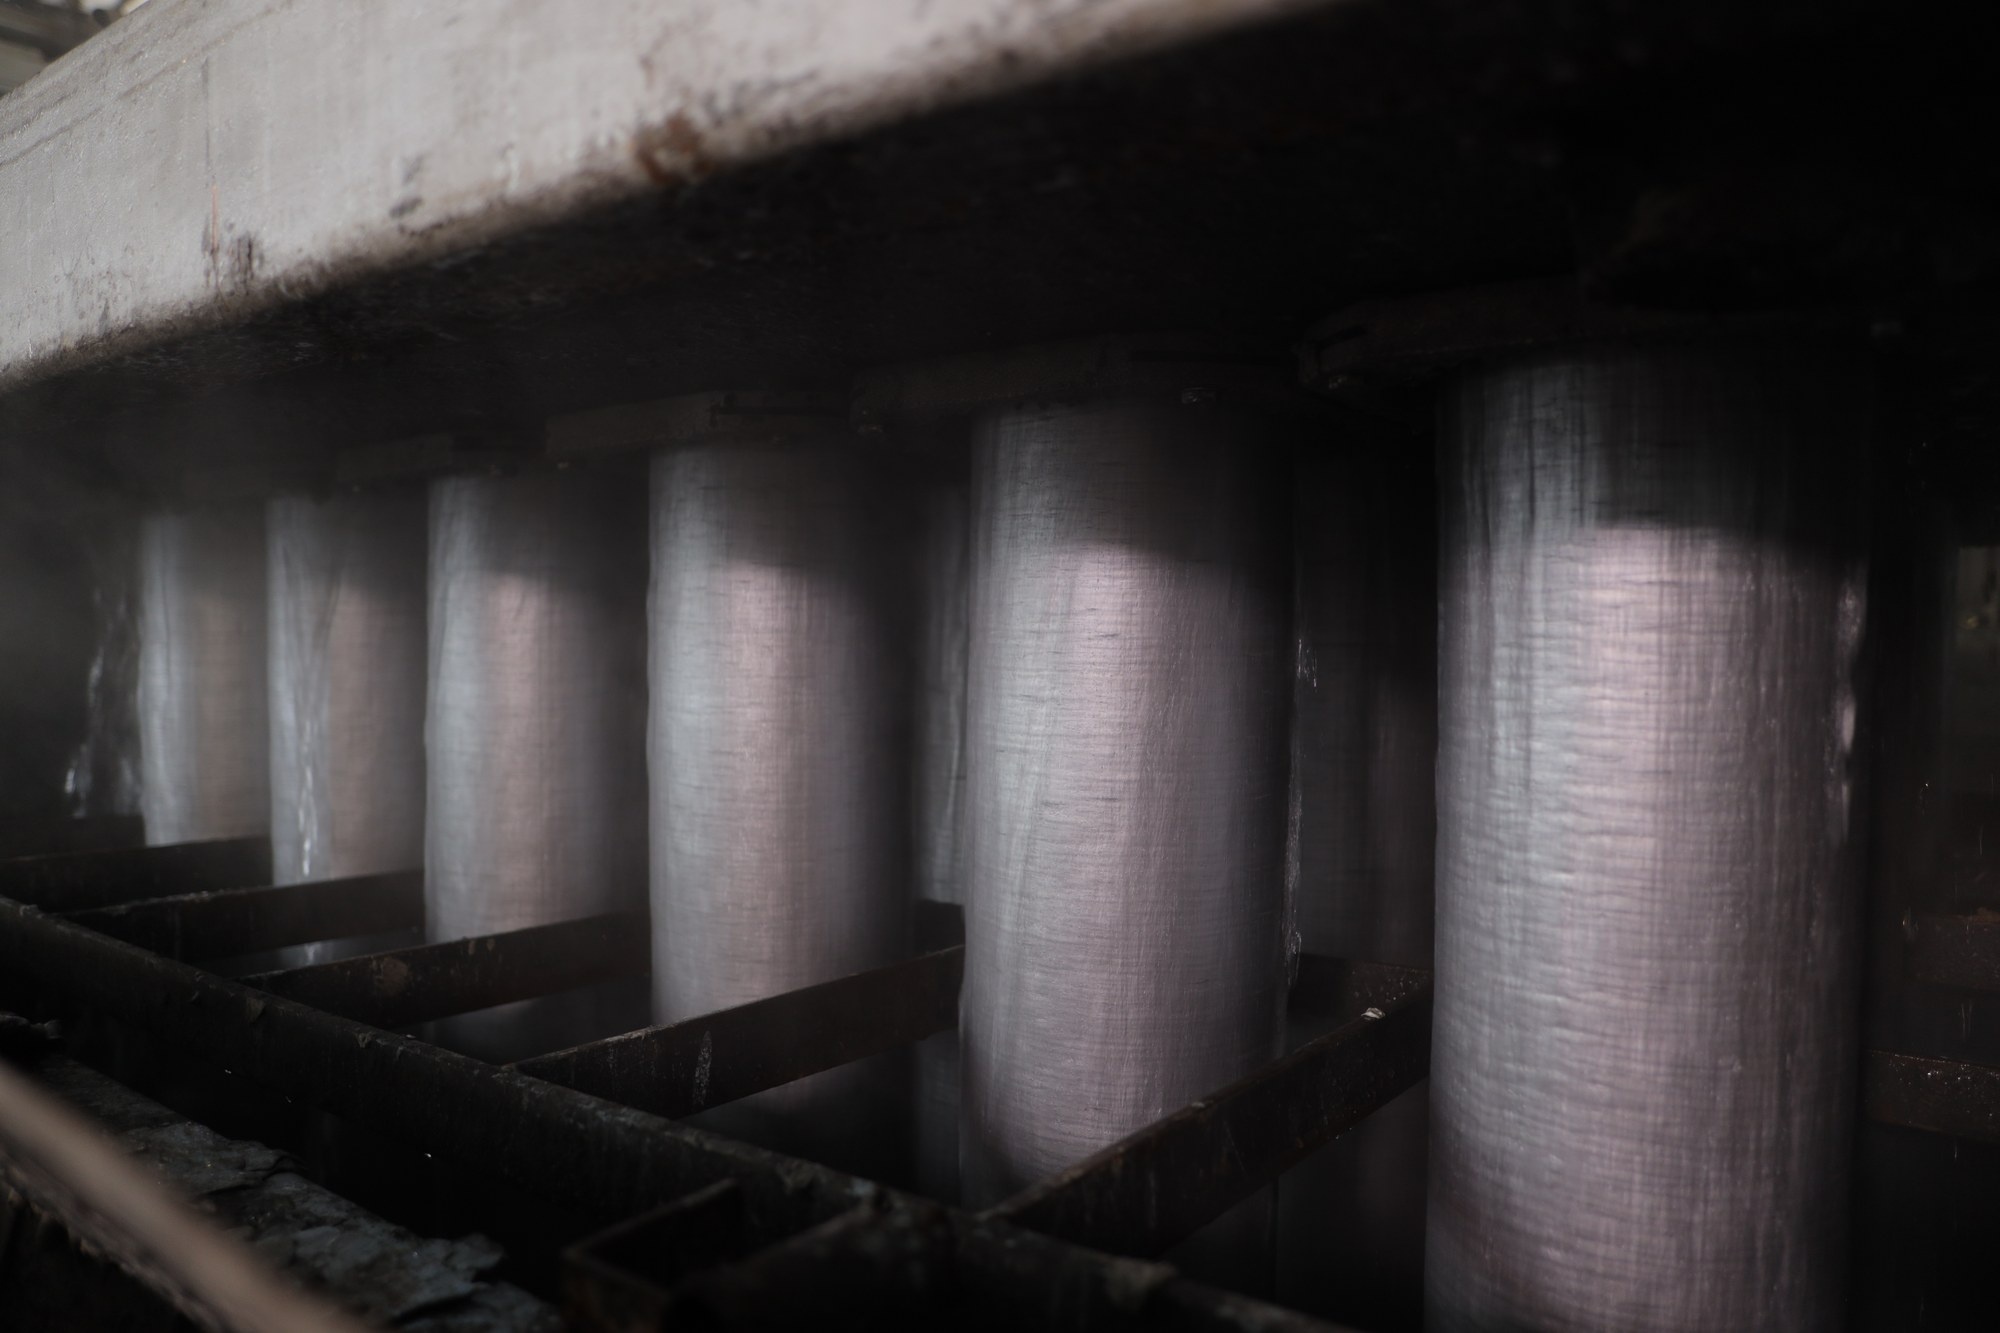
Hot-Top casting
Cylinder-guided Hot-Top casting controls casting speed and cooling rate with precision, delivering consistent surface finish, skin thickness, and metallurgical structure.
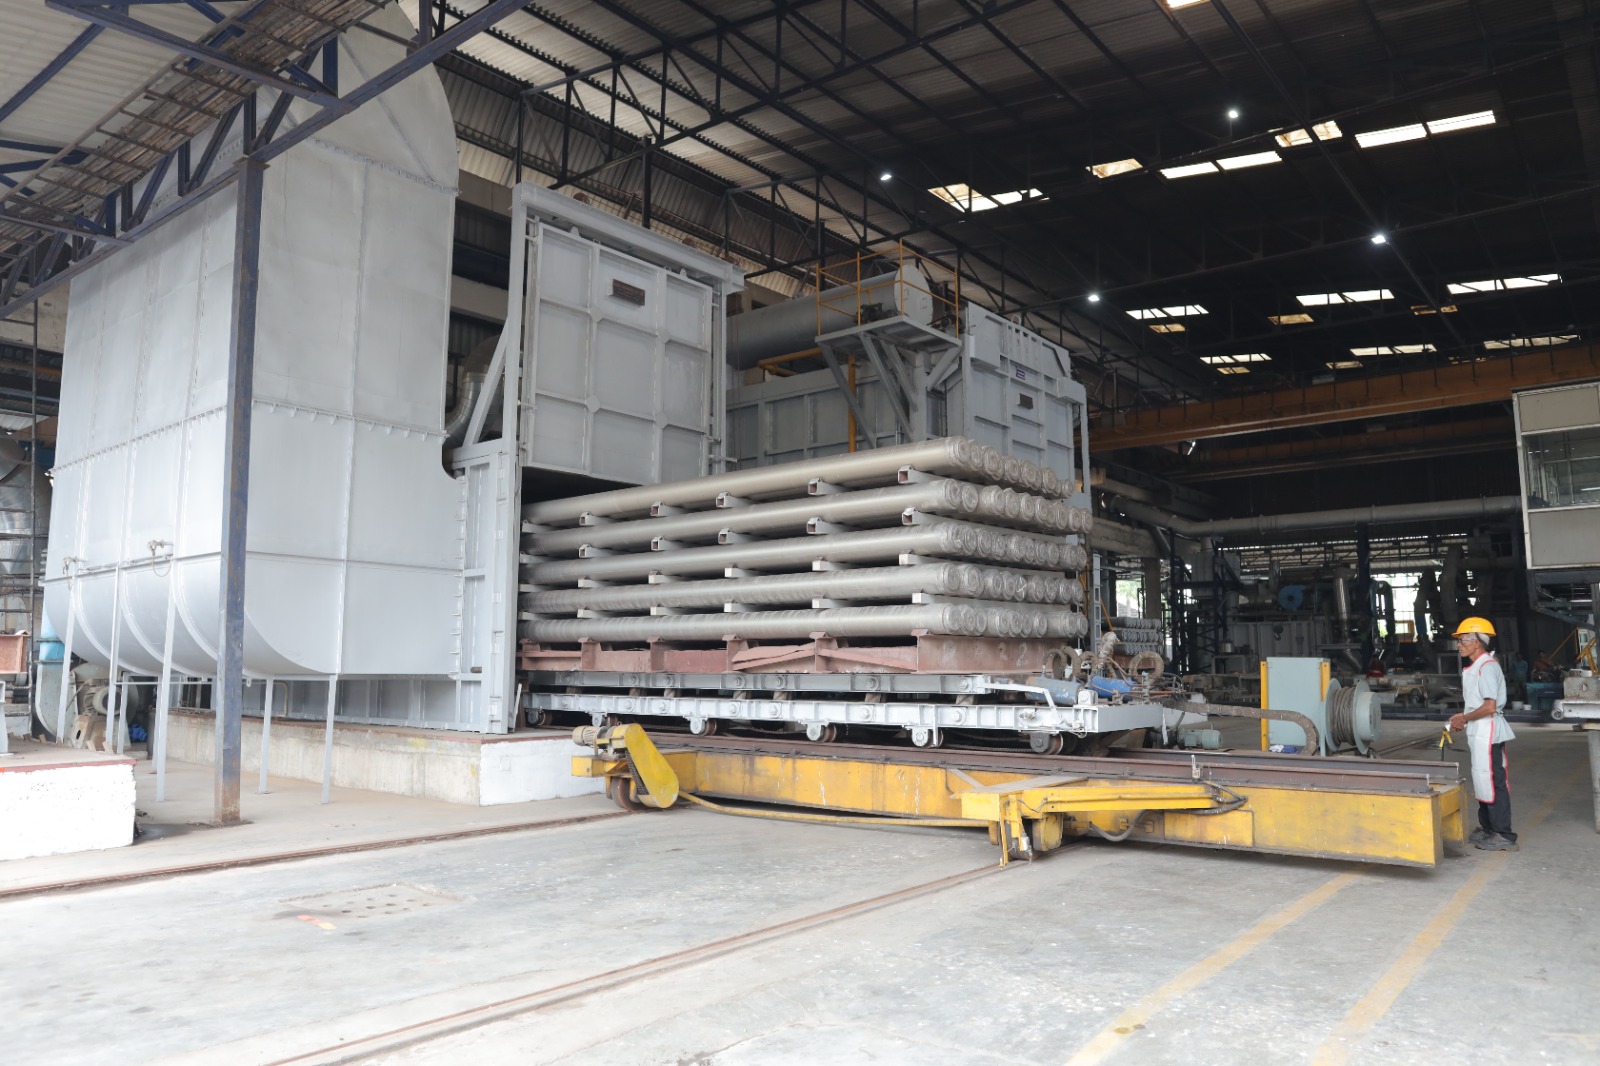
Homogenising
Controlled-atmosphere batch furnaces dissolve soluble phases and homogenise microstructure. Force-cooling to specified exit temperature governs extrudability and surface quality.
Need a specific composition?
Banco's in-house foundry team develops custom alloy compositions to customer specification, with specific Mg/Si ratios for anodising quality, lead-free conversions, and enhanced-machinability formulations.