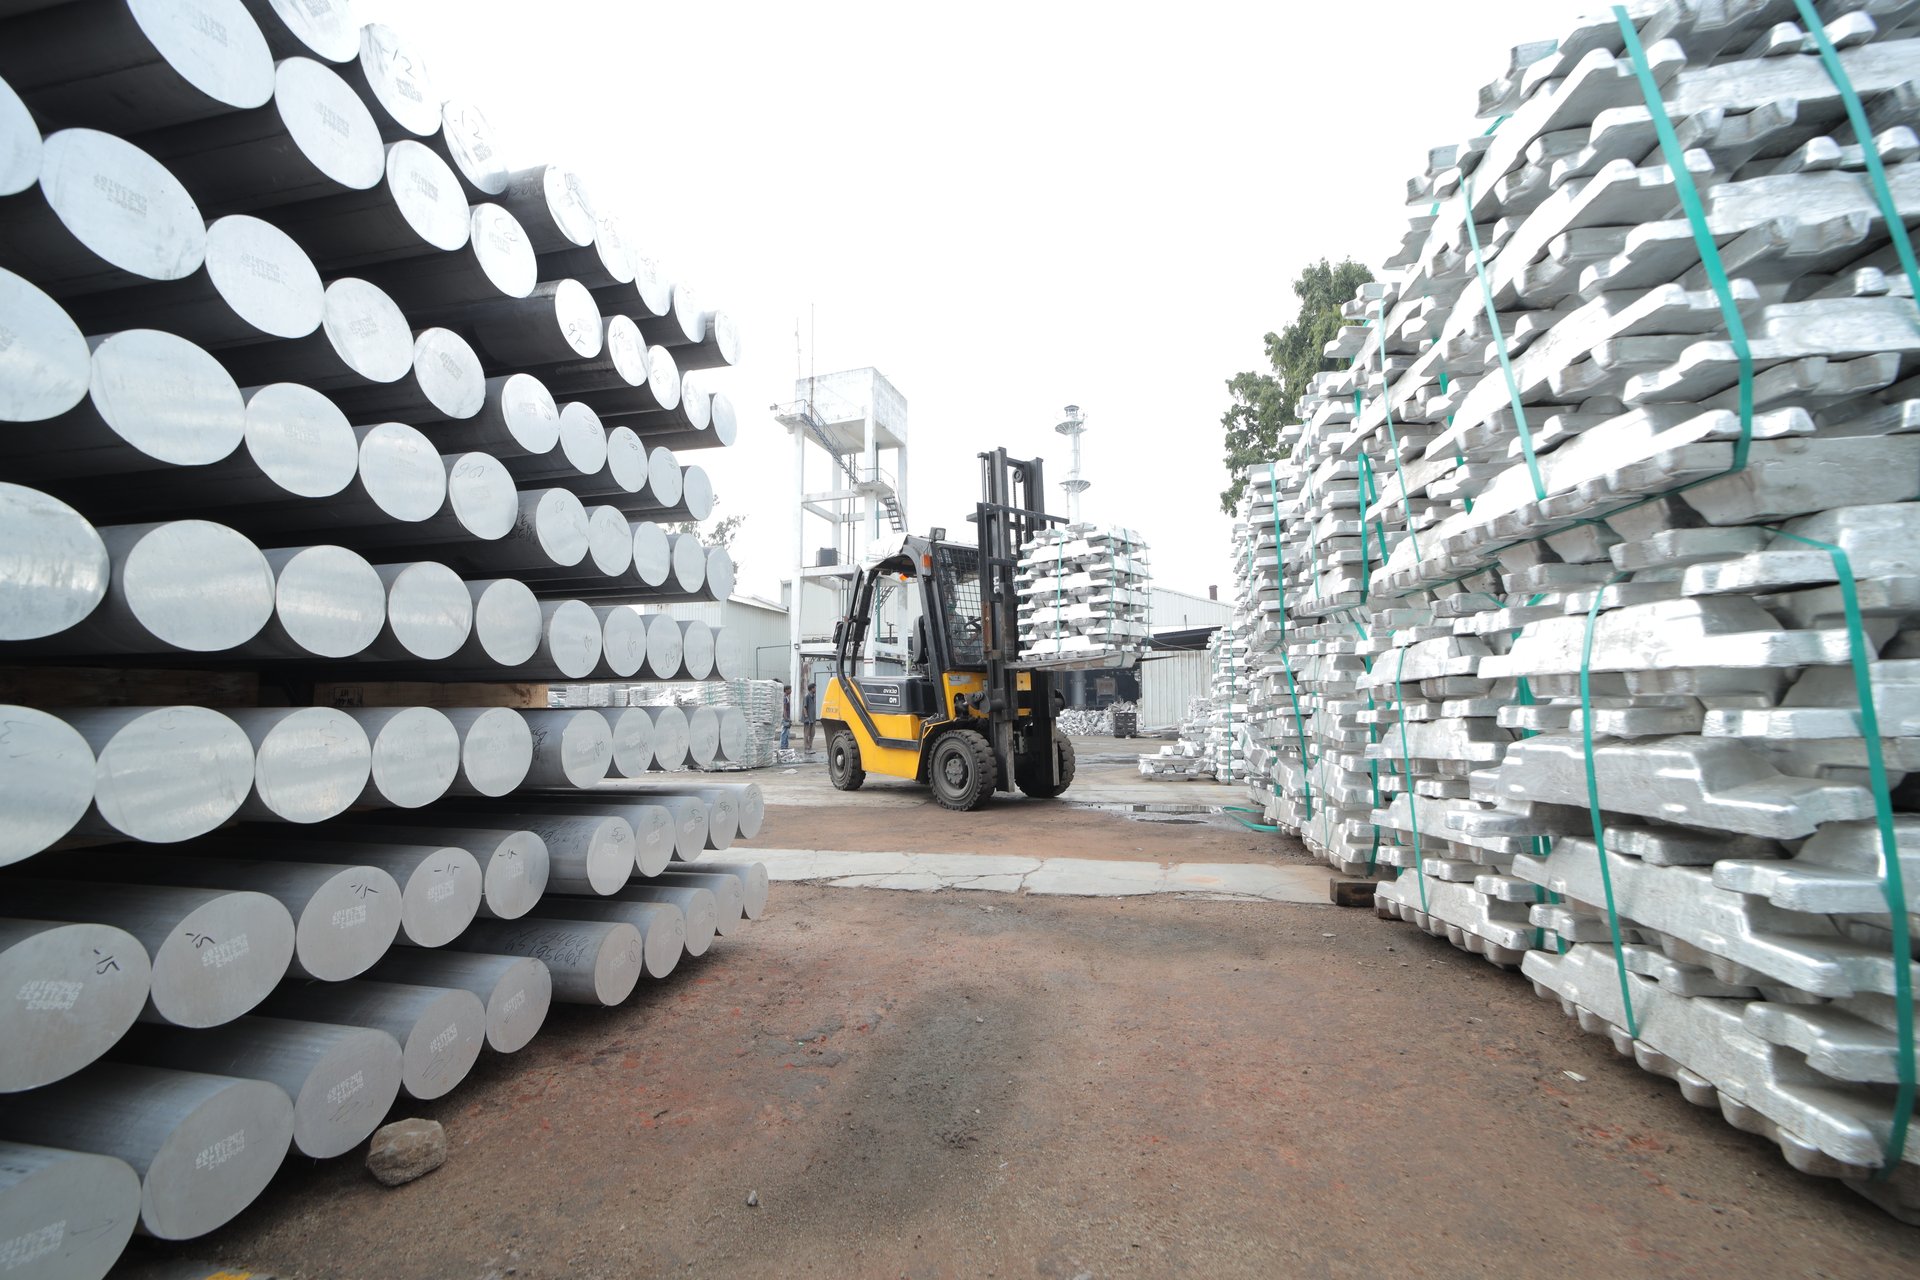
High Quality Extrusion Billets.
Wide range of Specification.
55,000 MT/yr
Foundry capacity
6 Diameters
5" to 10"
All Alloys
Custom on request
0.203 kgCO₂e/kg
ISO 14064-1 verified
Foundry · Billet production
Consistent metallurgical
quality, cast to cast.
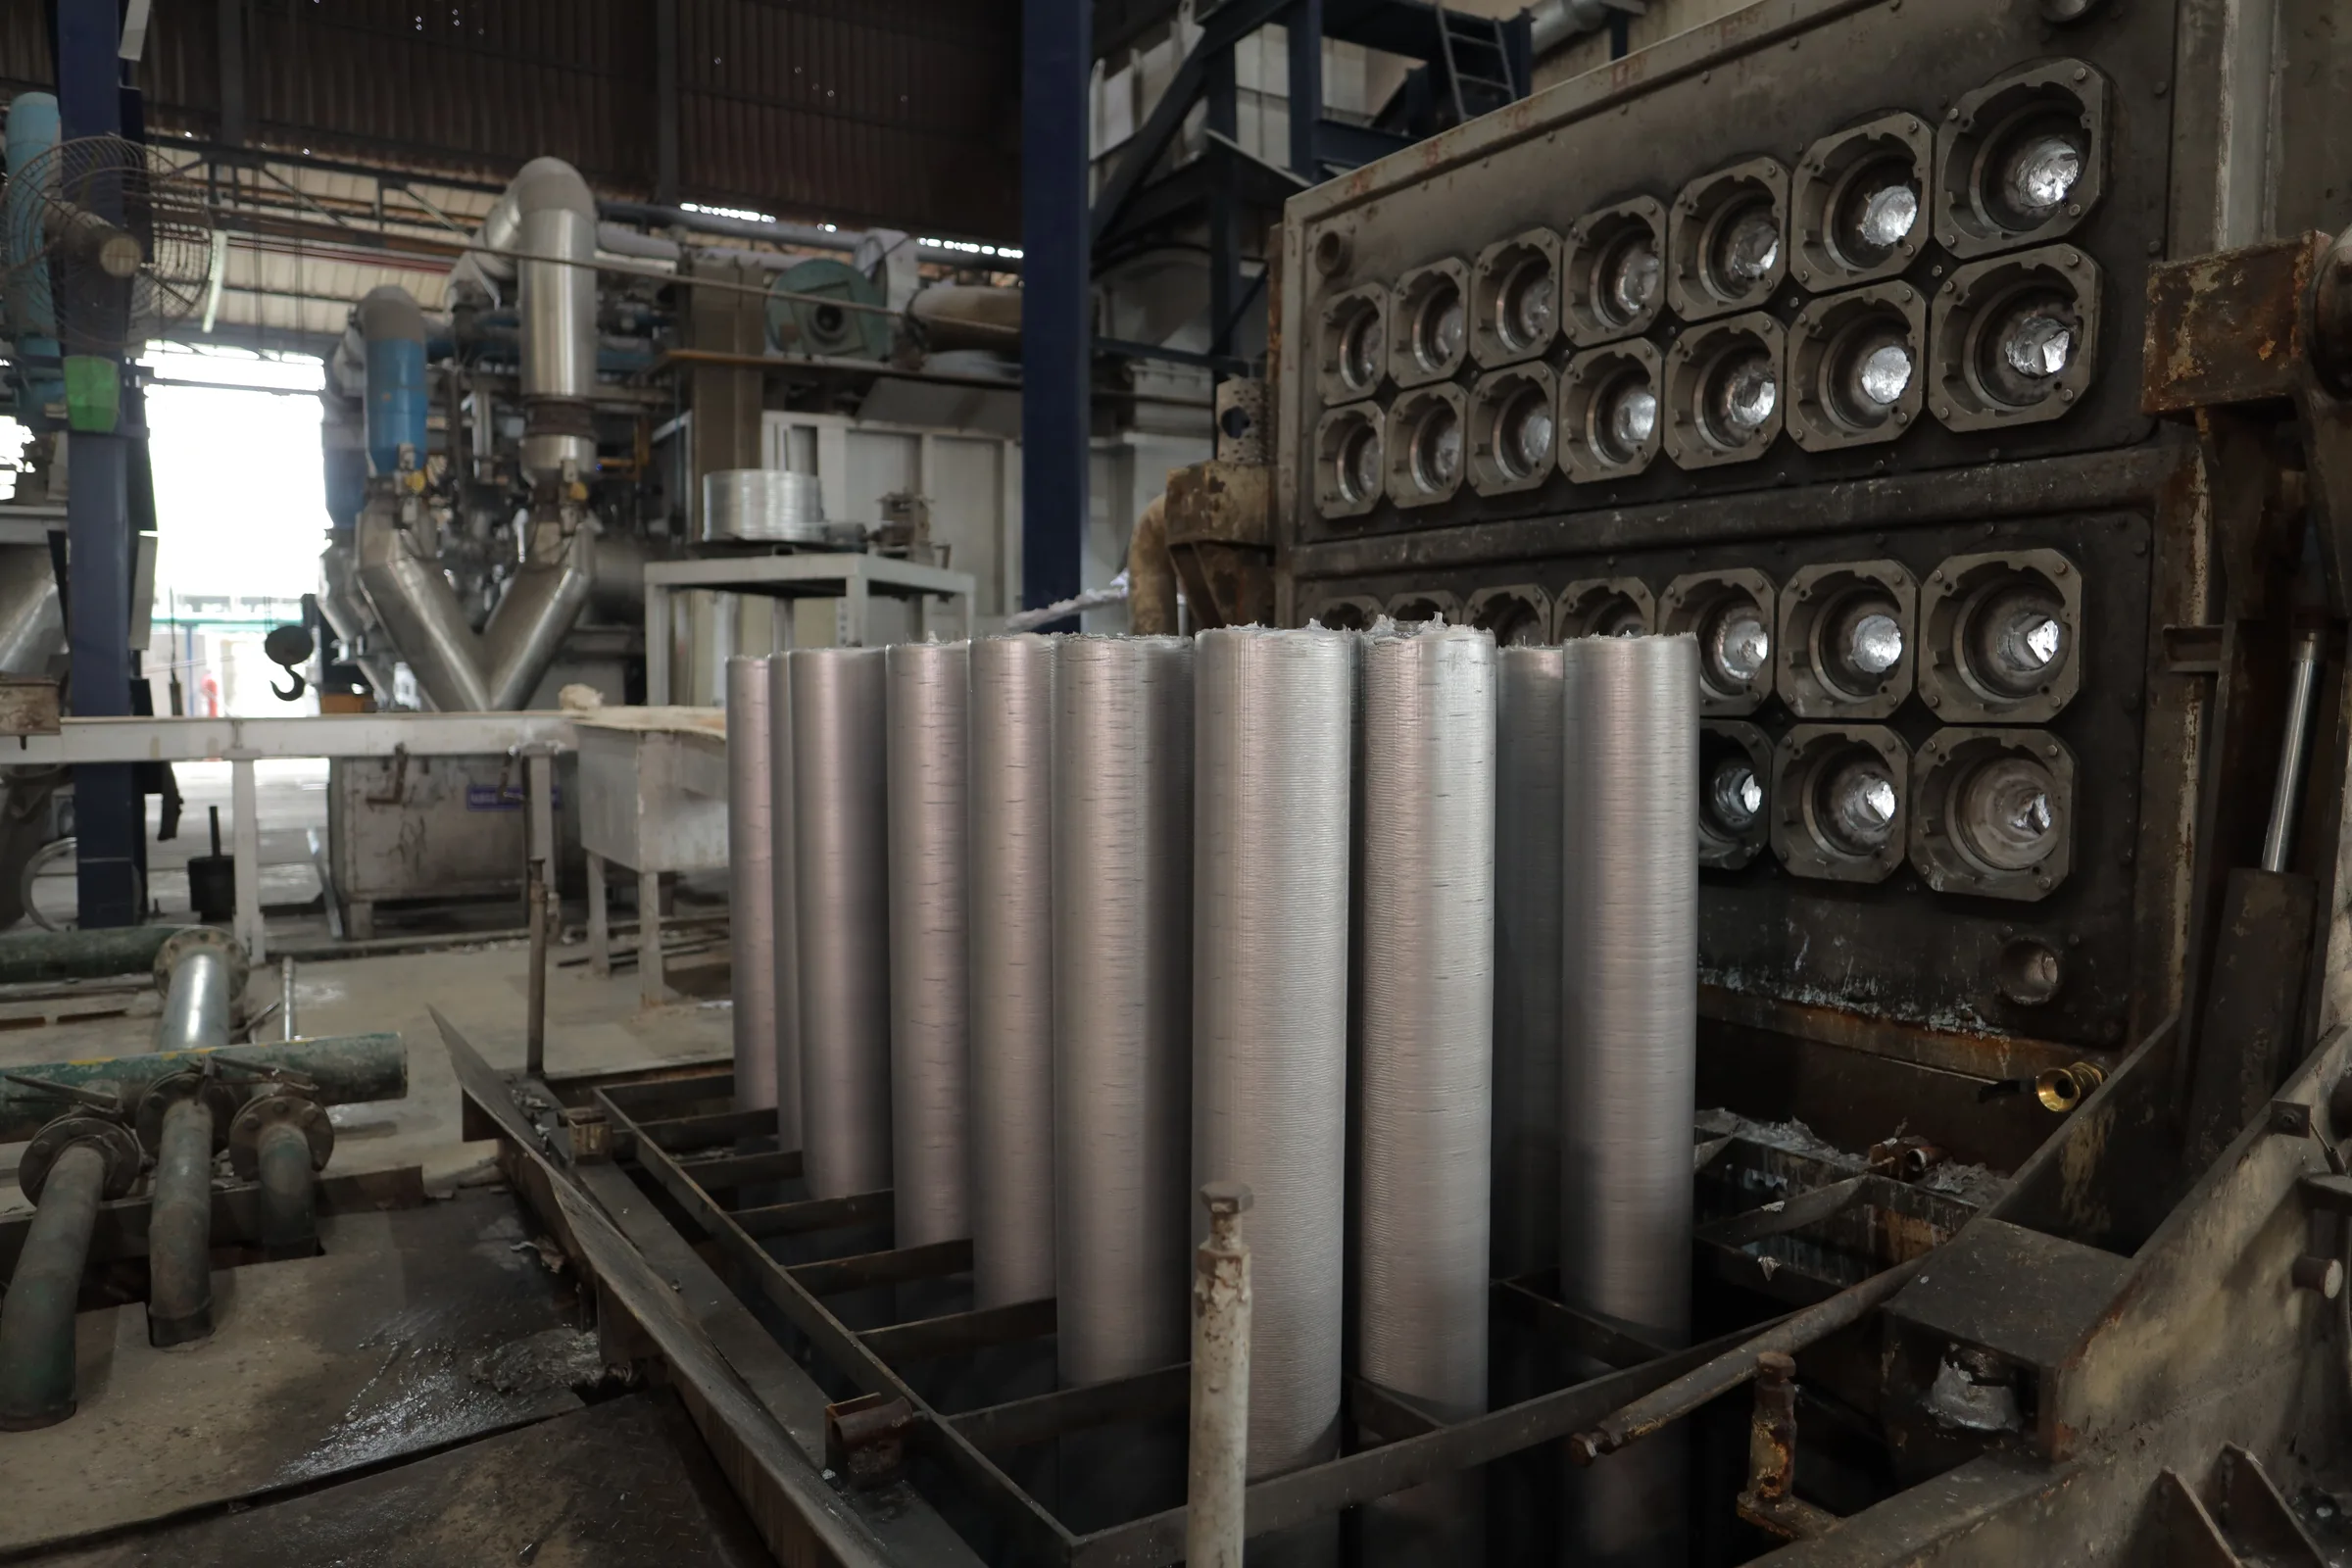
Banco's integrated foundry produces High Quality extrusion-grade aluminium billets using cylinder-guided Hot-Top casting, delivering controlled microstructure, measurable metal cleanliness and consistent extrudability, batch after batch.
Every billet undergoes 100% ultrasonic testing, spectroscopic chemical verification and full SCADA/ERP traceability from furnace charge through despatch.
Hot-Top castingIn-house alloy developmentSCADA/ERP traceabilityIQNETCBAM-readyExport-certified
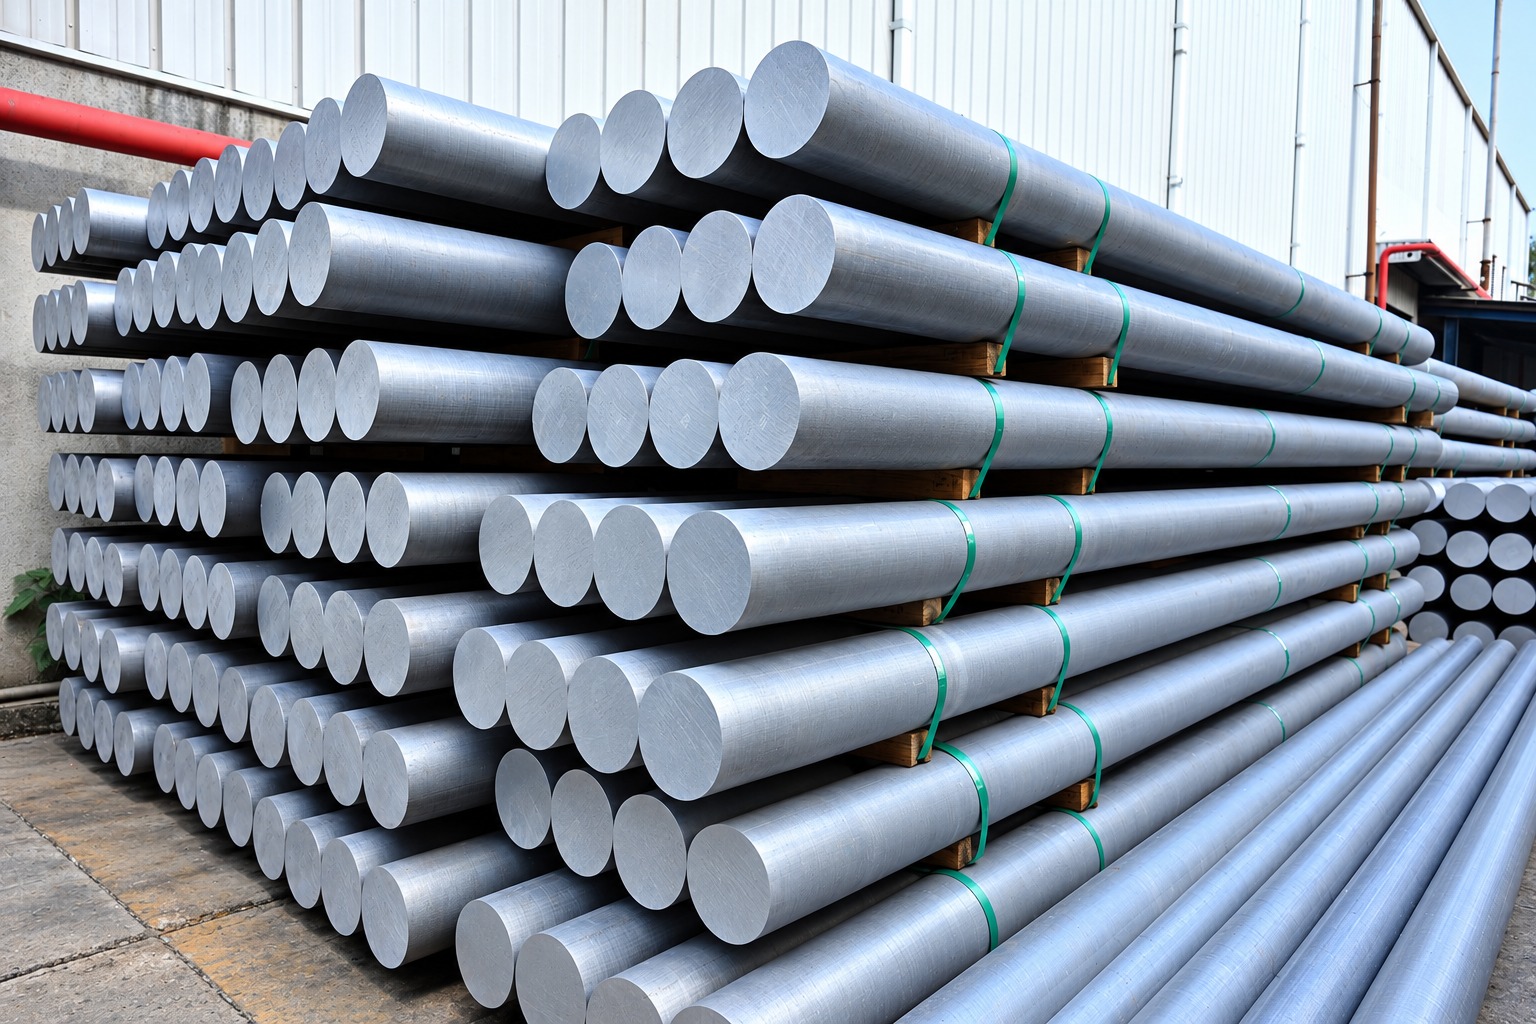
Finished extrusion billets Alloy-marked · 5,800 mm · SCADA/ERP traced
Standard alloys.
Custom compositions on request.
| Alloy | Si | Mg | Fe | Mn | Cu | Zn | Cr | Ti | Others each | Others total | Al | Remarks |
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 1050A | ≤ 0.25 | ≤ 0.05 | ≤ 0.40 | ≤ 0.05 | ≤ 0.05 | ≤ 0.07 | – | ≤ 0.05 | ≤ 0.03 | ≤ 0.10 | ≥ 99.50 | Conductivity & formability |
| 1070A | ≤ 0.20 | ≤ 0.03 | ≤ 0.25 | ≤ 0.03 | ≤ 0.03 | ≤ 0.07 | – | ≤ 0.03 | ≤ 0.03 | ≤ 0.10 | ≥ 99.70 | Higher electrical conductivity |
| 1100 | Si+Fe ≤ 0.95 | – | Si+Fe ≤ 0.95 | ≤ 0.05 | 0.05–0.20 | – | – | – | ≤ 0.05 | ≤ 0.15 | ≥ 99.00 | Excellent corrosion resistance |
| 2014 | 0.50–1.20 | 0.20–0.80 | ≤ 0.70 | 0.40–1.20 | 3.90–5.00 | ≤ 0.25 | ≤ 0.10 | ≤ 0.15 | ≤ 0.05 | ≤ 0.15 | Remainder | Very high strength |
| 2017A | 0.20–0.80 | 0.40–1.00 | ≤ 0.70 | 0.40–1.00 | 3.50–4.50 | ≤ 0.25 | ≤ 0.10 | – | ≤ 0.05 | ≤ 0.15 | Remainder | Zr+Ti = 0.25 max · High strength & machinability |
| 3003 | ≤ 0.60 | – | ≤ 0.70 | 1.00–1.50 | 0.05–0.20 | ≤ 0.10 | – | – | ≤ 0.05 | ≤ 0.15 | Remainder | Good formability and corrosion resistance |
| 6101 | 0.30–0.70 | 0.35–0.80 | ≤ 0.50 | ≤ 0.03 | ≤ 0.10 | ≤ 0.10 | ≤ 0.03 | – | ≤ 0.03 | ≤ 0.10 | Remainder | Electrical conductor grade |
| 6060 | 0.30–0.60 | 0.35–0.60 | 0.10–0.30 | ≤ 0.10 | ≤ 0.10 | ≤ 0.15 | ≤ 0.05 | ≤ 0.10 | ≤ 0.05 | ≤ 0.10 | Remainder | Architectural profiles |
| 6063 | 0.20–0.60 | 0.45–0.90 | ≤ 0.35 | ≤ 0.10 | ≤ 0.10 | ≤ 0.10 | ≤ 0.10 | ≤ 0.10 | ≤ 0.05 | ≤ 0.15 | Remainder | Windows / doors / general extrusion |
| 6005 | 0.60–0.90 | 0.40–0.60 | ≤ 0.35 | ≤ 0.10 | ≤ 0.10 | ≤ 0.10 | ≤ 0.10 | ≤ 0.10 | ≤ 0.05 | ≤ 0.15 | Remainder | Medium strength structural / solar frame applications |
| 6005A | 0.50–0.90 | 0.40–0.70 | ≤ 0.35 | ≤ 0.50 | ≤ 0.30 | ≤ 0.20 | ≤ 0.30 | ≤ 0.10 | ≤ 0.05 | ≤ 0.15 | Remainder | Mn+Cr = 0.12–0.50 · Transport / structural |
| 6082 | 0.70–1.30 | 0.60–1.20 | ≤ 0.50 | 0.40–1.00 | ≤ 0.10 | ≤ 0.20 | ≤ 0.25 | ≤ 0.10 | ≤ 0.05 | ≤ 0.15 | Remainder | High strength structural |
| 6351 | 0.70–1.30 | 0.40–0.80 | ≤ 0.50 | 0.40–0.80 | ≤ 0.10 | ≤ 0.20 | – | ≤ 0.20 | ≤ 0.05 | ≤ 0.15 | Remainder | High strength for pressure applications |
| 6061 | 0.40–0.80 | 0.80–1.20 | ≤ 0.70 | ≤ 0.15 | 0.15–0.40 | ≤ 0.25 | 0.04–0.35 | ≤ 0.15 | ≤ 0.05 | ≤ 0.15 | Remainder | Engineering / aerospace |
| 6066 | 0.90–1.80 | 0.80–1.40 | ≤ 0.50 | 0.60–1.10 | 0.70–1.20 | ≤ 0.25 | ≤ 0.40 | ≤ 0.20 | ≤ 0.05 | ≤ 0.15 | Remainder | High-strength forgings |
1xxx, 2xxx, 3xxx, 6xxx, and 7xxx series, along with any special compositions, are all available to customer specifications.
Hard and high-strength alloys for structural, transport, defence, aerospace and engineering applications
Lead-free free-machining alloys, including 6026, for automotive, medical, food processing and precision-machined components
Electrical conductivity alloys for busbars and conductor profiles
Custom alloys and special chemistries developed as per customer specification
Six diameters.
5,800 mm standard length.
Available diameters
127 mm
5"
Standard residential extrusion
152 mm
6"
Window · door systems
178 mm
7"
Commercial structural profiles
203 mm
8"
Heavy-section industrial profiles
229 mm
9"
Heavy-duty industrial sections
254 mm
10"
Large-section · press 4 & 5
Dimensional tolerances
Diameter
± 1% of nominal diameter
Length
± 5 mm
Bow / camber
≤ 2 mm per metre · ≤ 10 mm full length
Cutting angle
90° ± 0.5°
Std. length
5,800 mm (all diameters)
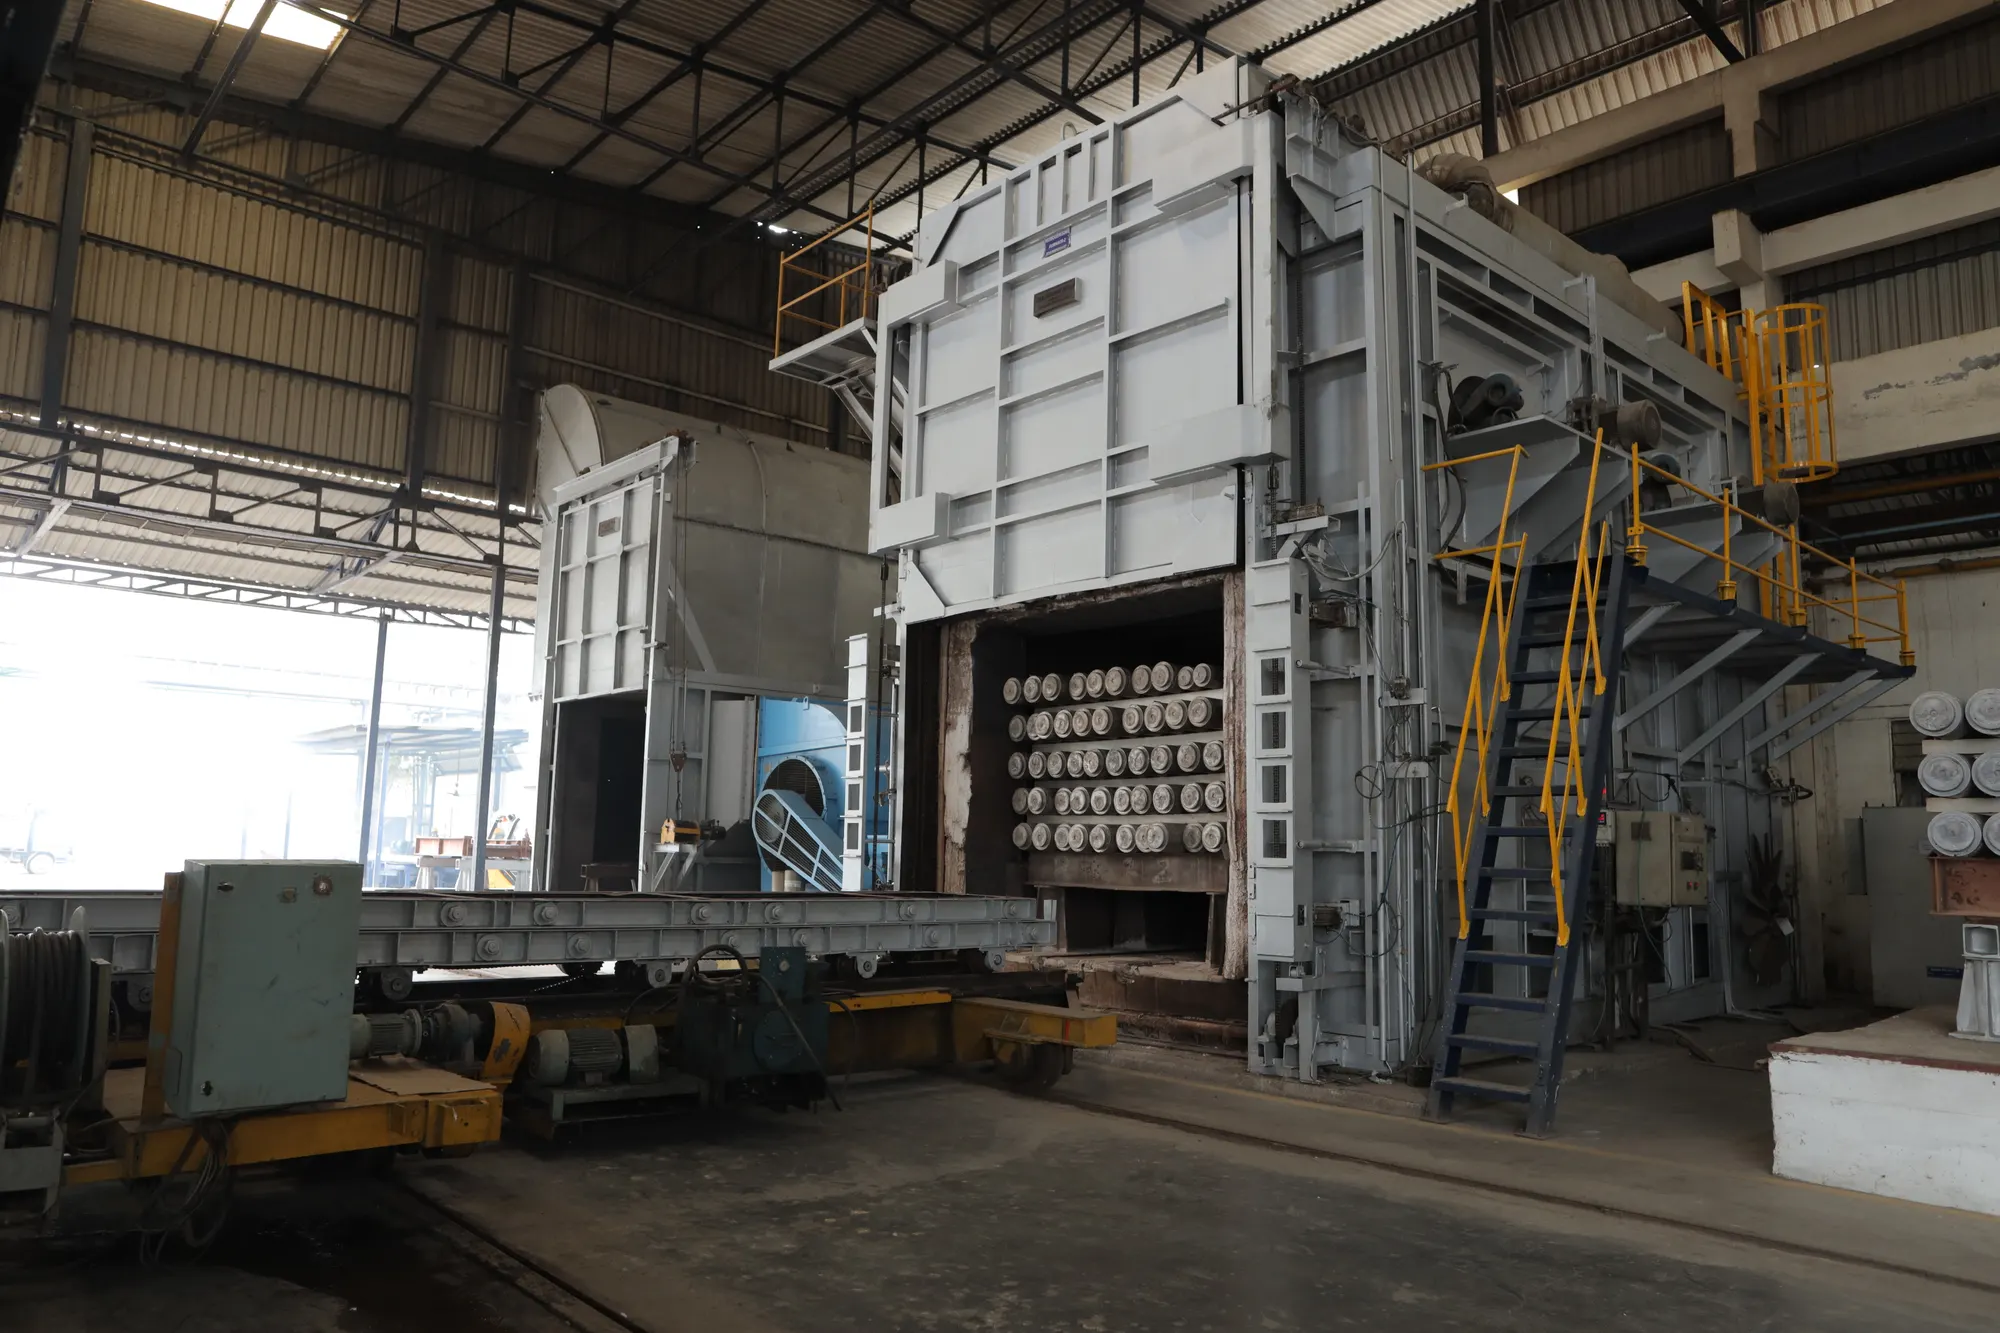
From melt to billet.
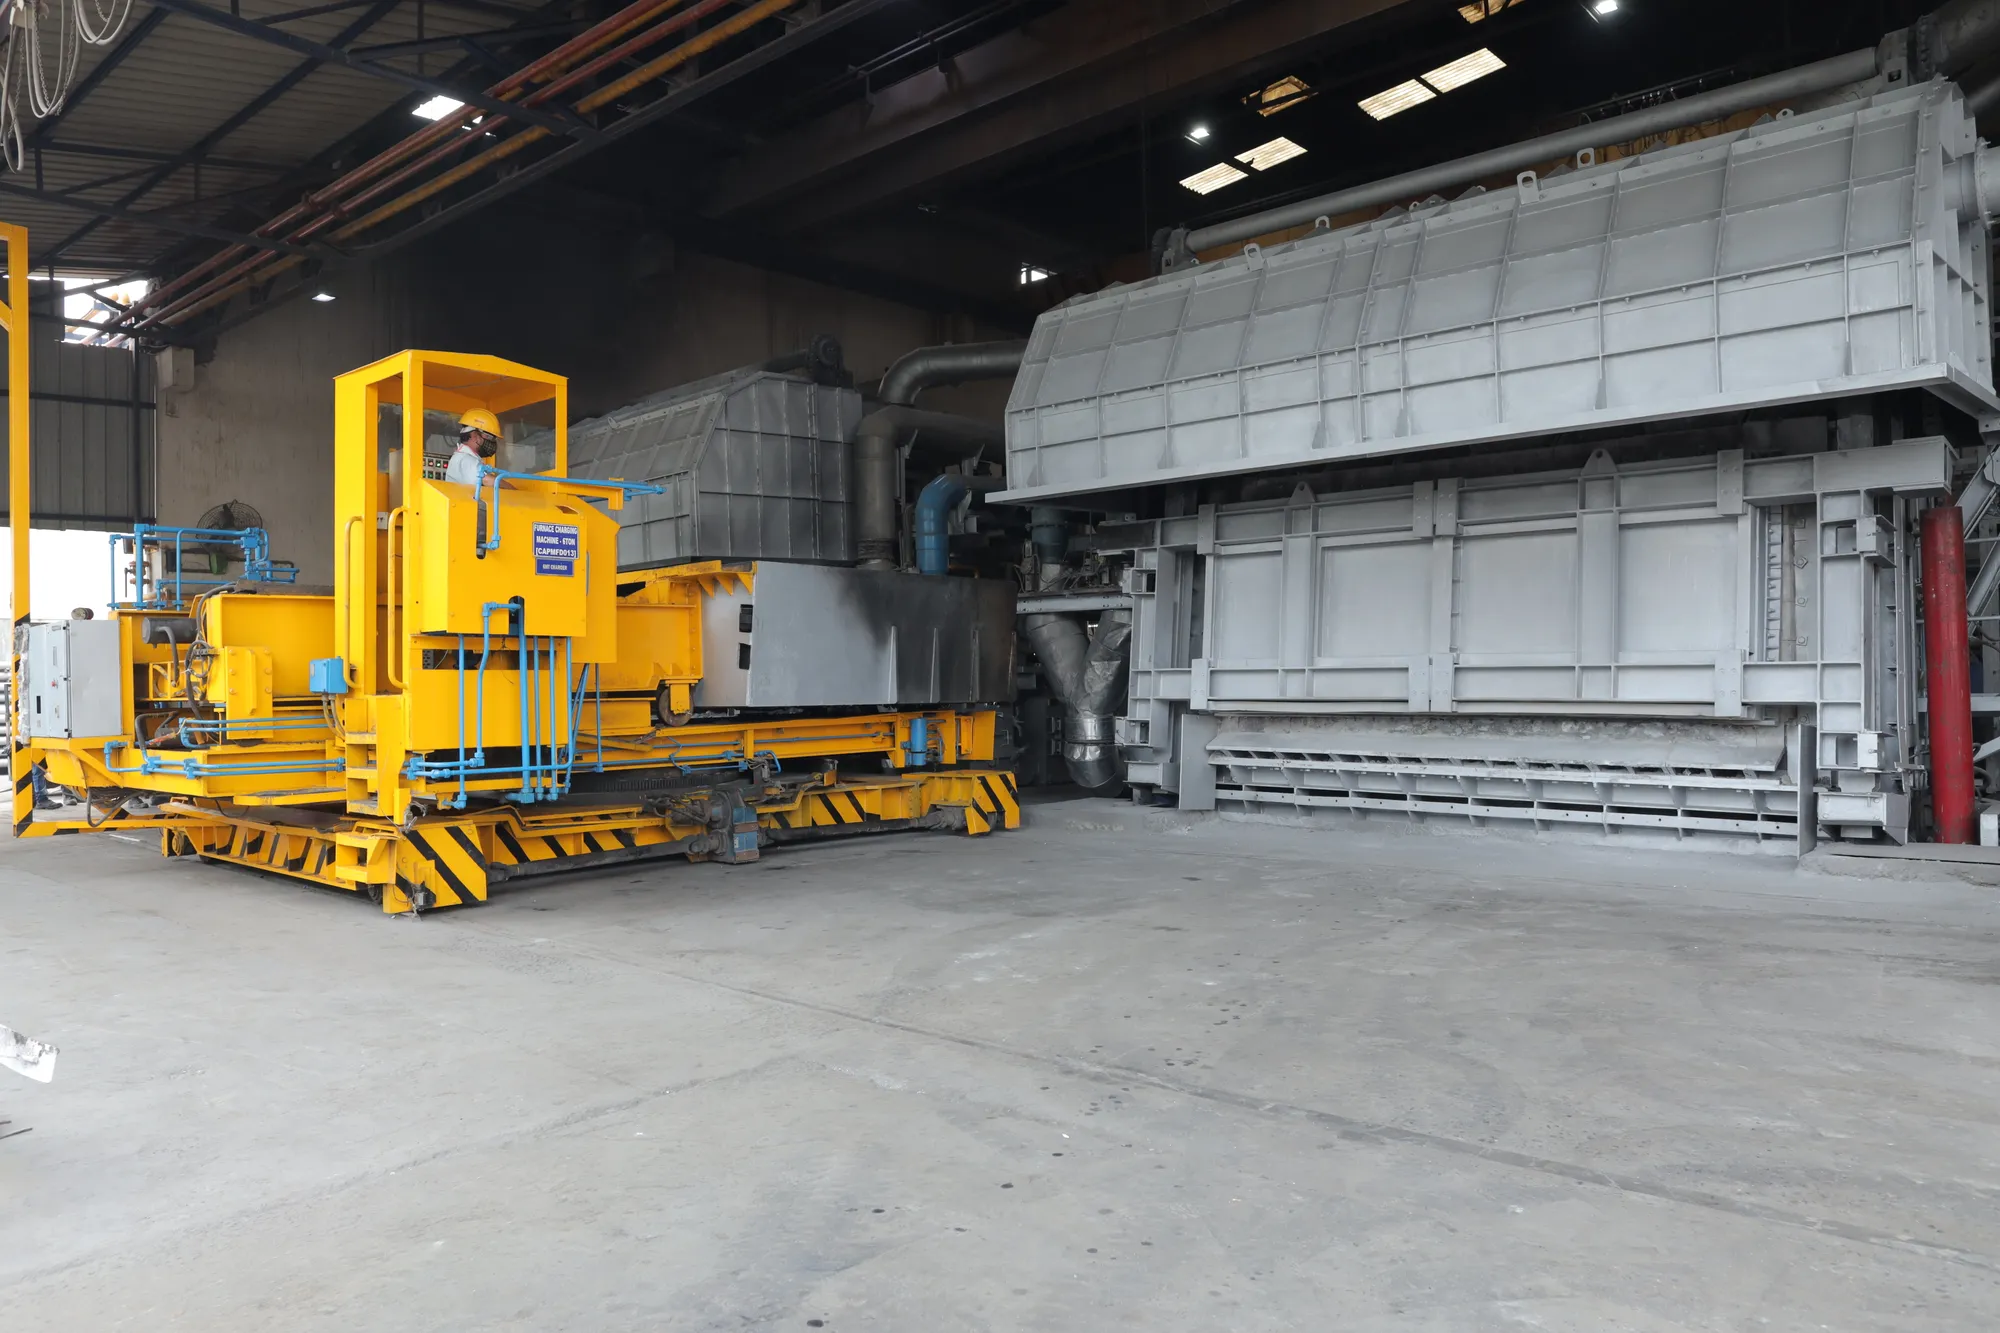
/ 01
Melting
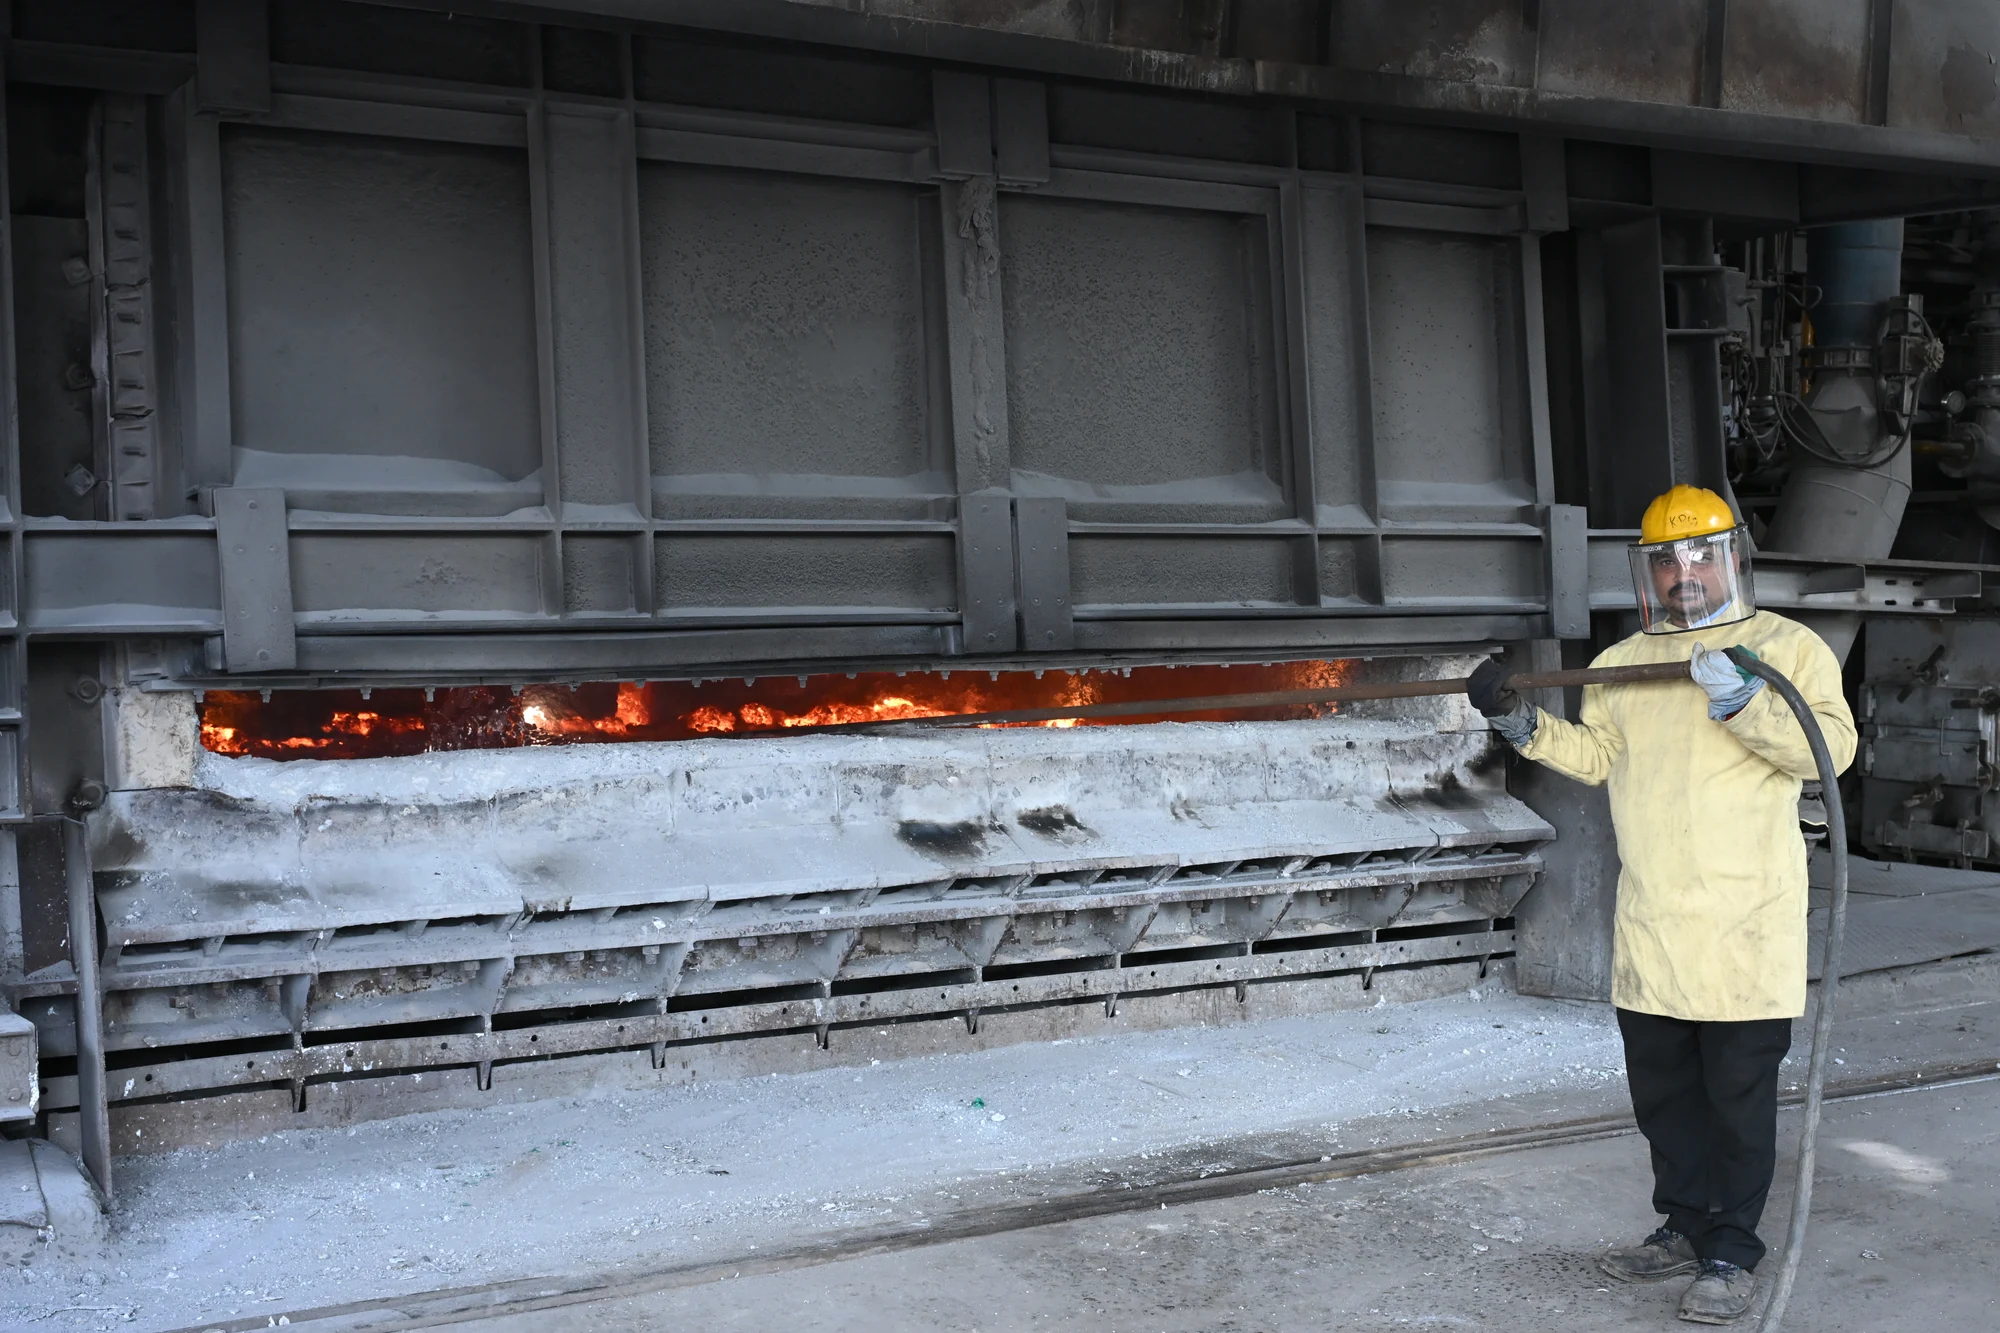
/ 02
Refining & degassing
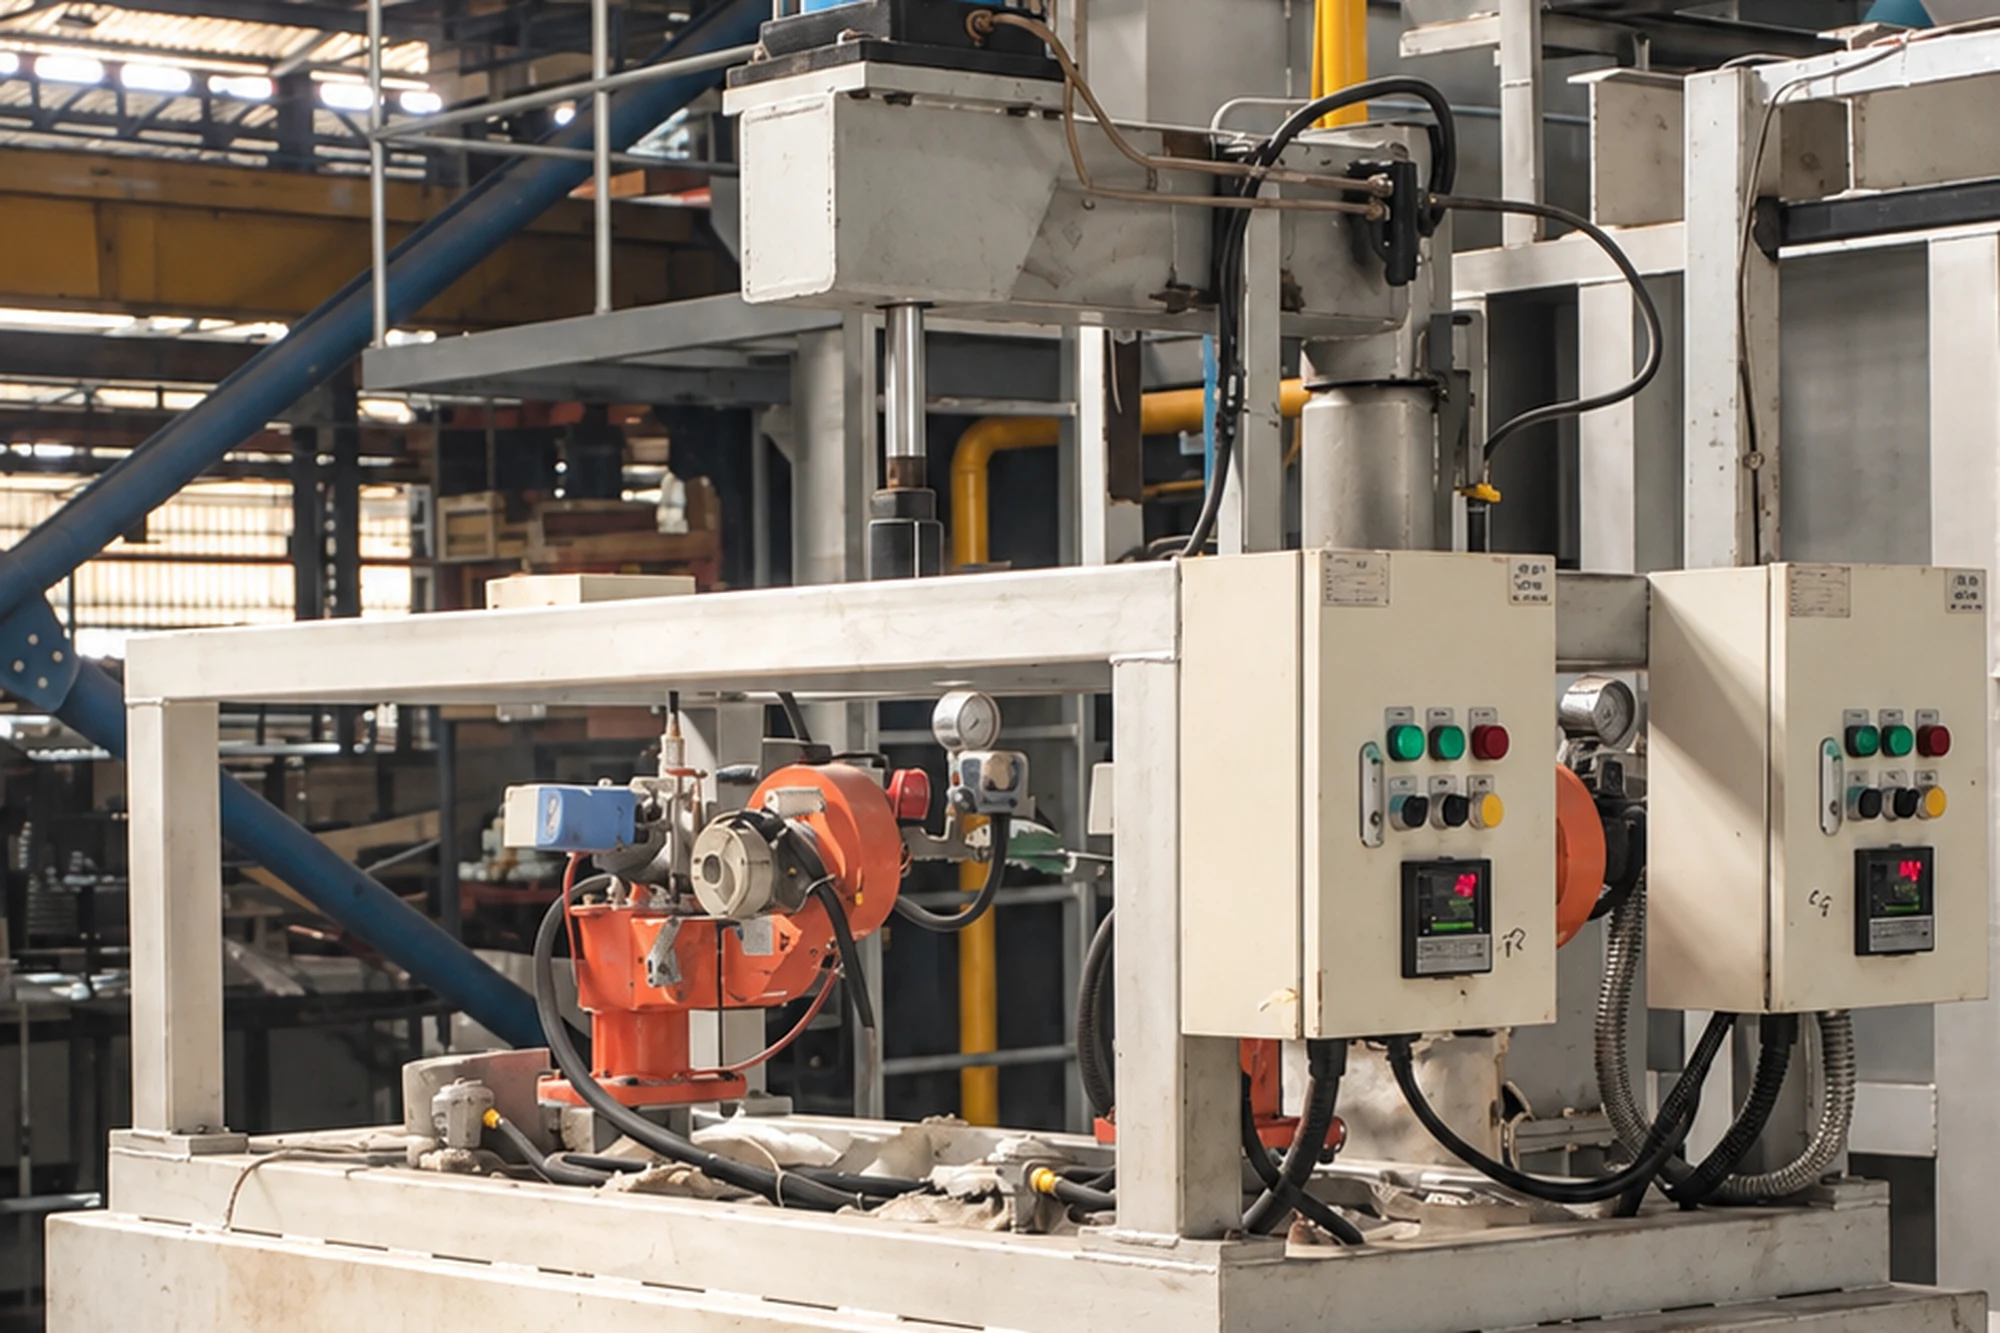
/ 03
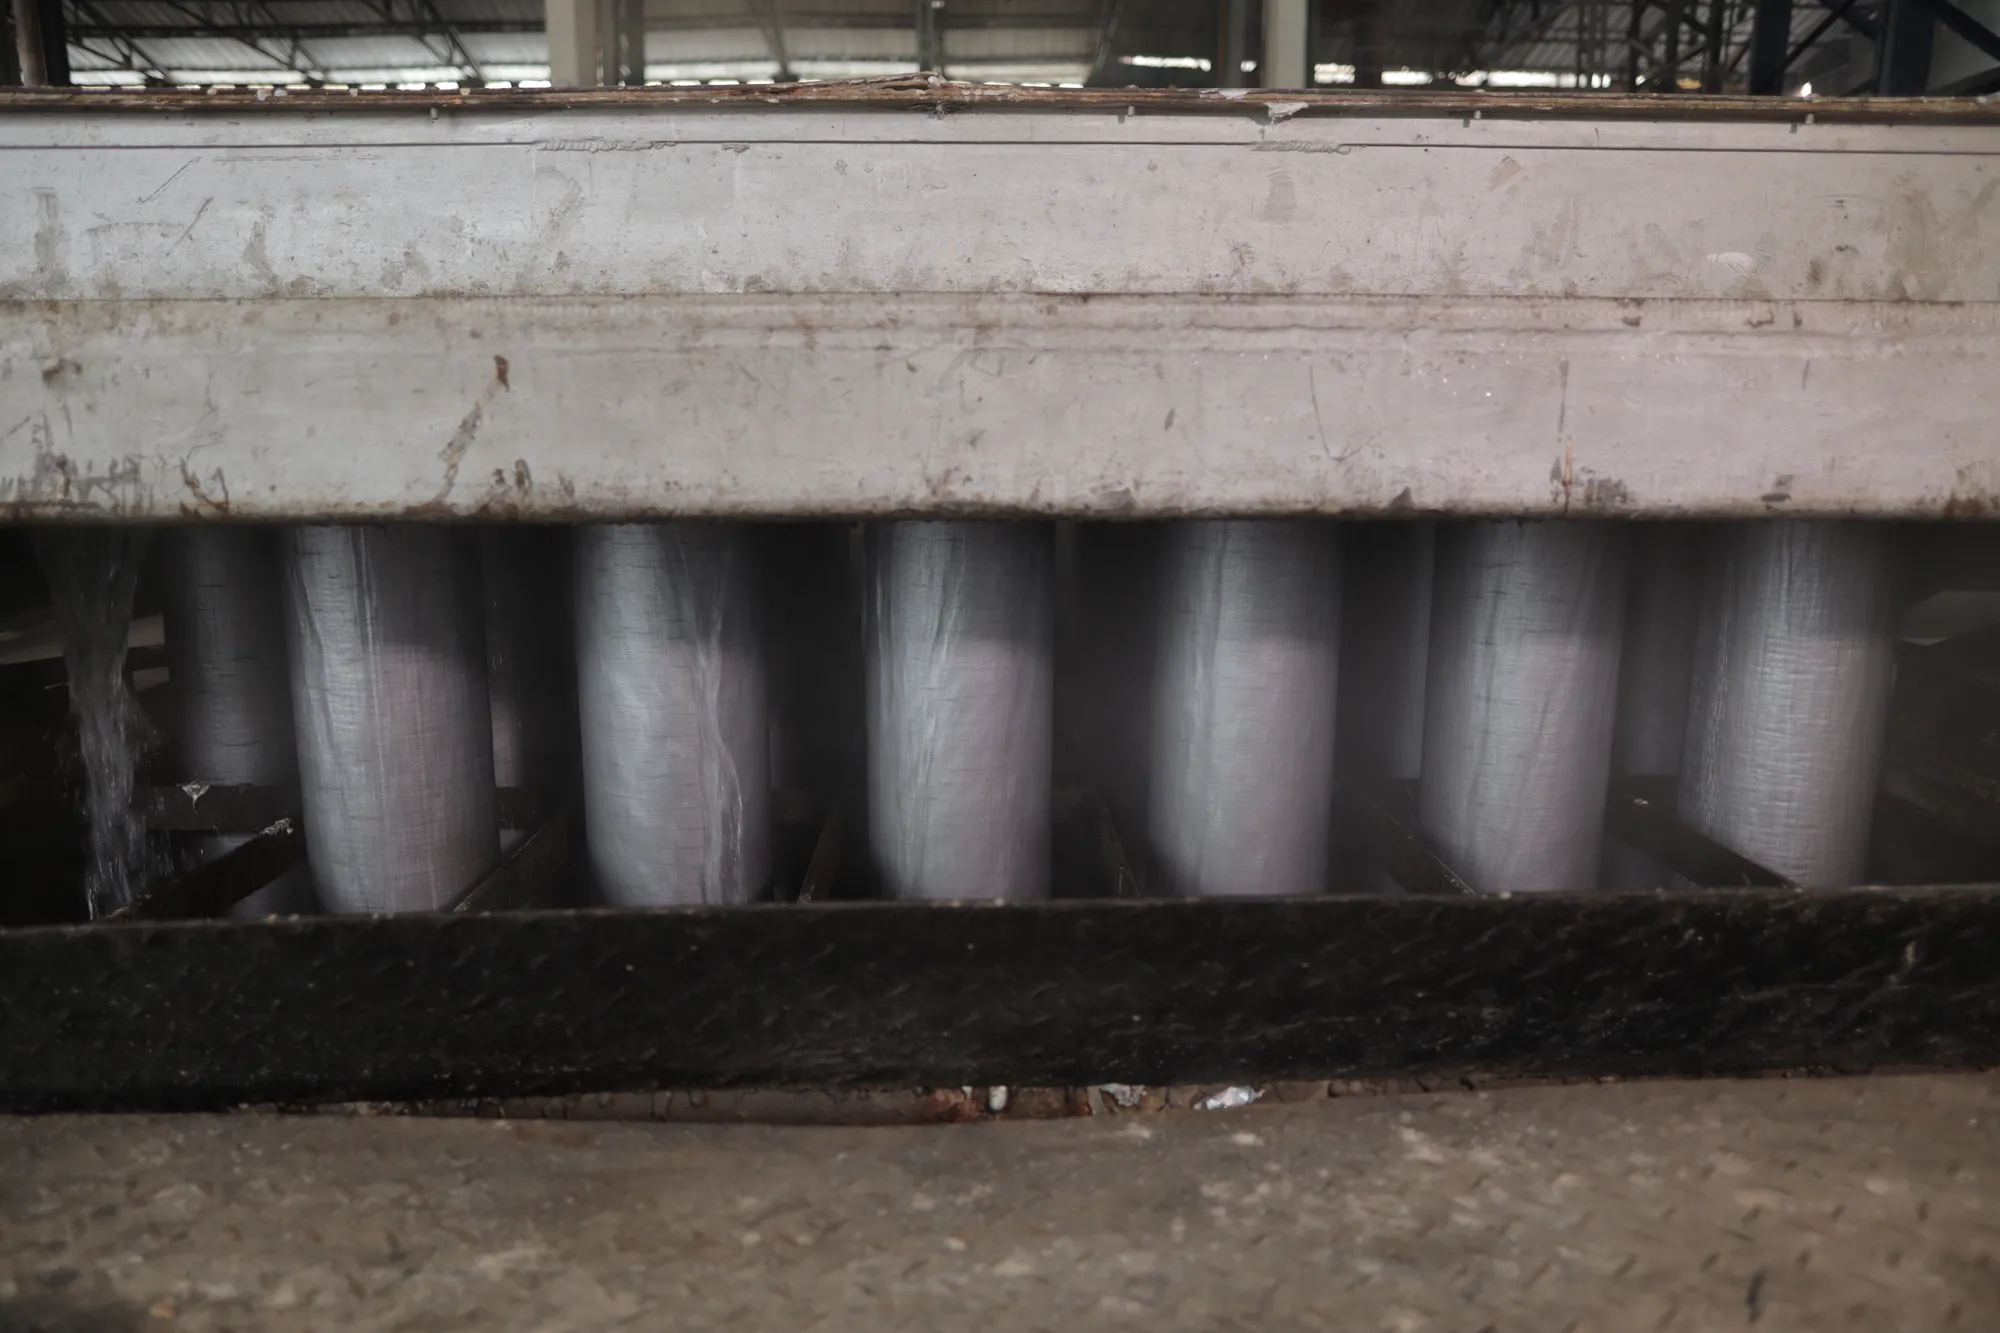
Ceramic foam filtration
/ 04
Hot-Top casting
/ 05
Batch homogenising
100% inspection
at every stage.
100 %
Visual inspection for external defects
External surface; every billet, every cast
100 %
Ultrasonic testing
Internal defects: inclusions, voids
100 %
Chemical analysis
Spectromax OES, verified against order specification
SCADA/ERP
Online traceability
Furnace conditions to despatch, batch-linked
Alloy marking
Unique Cast No.
Designation + cast number on every individual billet
Ceramic filtration
Inline grain refinement
Fine, uniform, equiaxed crystal structure
Packing
0.203 kgCO₂e/kg.
ISO 14064-1 verifiedCBAM documentationUp to 95% recycled input for green billets960 kW integrated captive solarNatural gas melting
≤ 5%
Verified primary aluminium in green billet grade
960 kW
Captive solar generation on site
100%
Natural gas in melting